M.H. – Material Handling

Efficiency improvement of the lines

On this blog, I often discuss packaging process optimization and the machinery that can be installed to achieve this goal. Designing a line from scratch, perhaps even with ample space available, is one thing; intervening on an existing line with its mechanisms already in motion is another.

Is it still possible to optimize the process in these cases? Good question! The answer is yes, but there are multiple paths to take.

Today, I want to outline some solutions to this issue because more and more companies already have a packaging line but need to make it more efficient, both in terms of performance and ergonomics.

Recently, we’ve encountered many with this problem… just think of the contacts we made during Cibus Tec at the end of 2023.

What do these production realities need?

  1. To gain space in facilities where square meters are limited and often fully utilized.
  2. To increase packaging speed.
  3. To free up floor space and develop the process vertically (returning to point 1).
  4. To make the phase from primary to secondary packaging more efficient.
  5. To adapt to changes related to seeking greater sustainability in processes.

What are the solutions in these cases?

T o create overpasses and free up floor space, some technologically advanced solutions can be introduced, such as:

  • Operator passages with gate-opening belts;
  • Retractable systems;
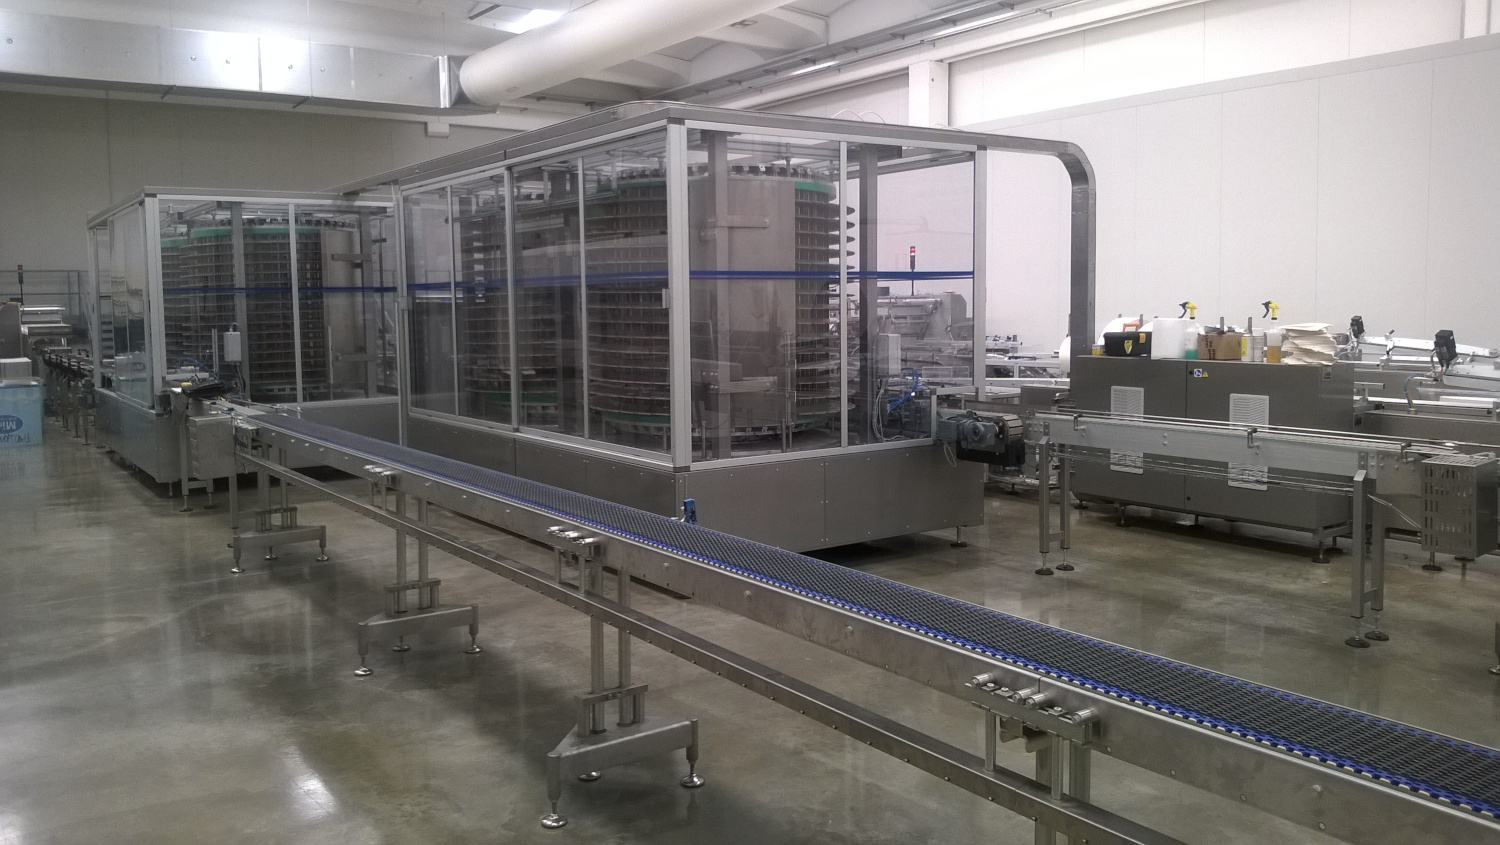
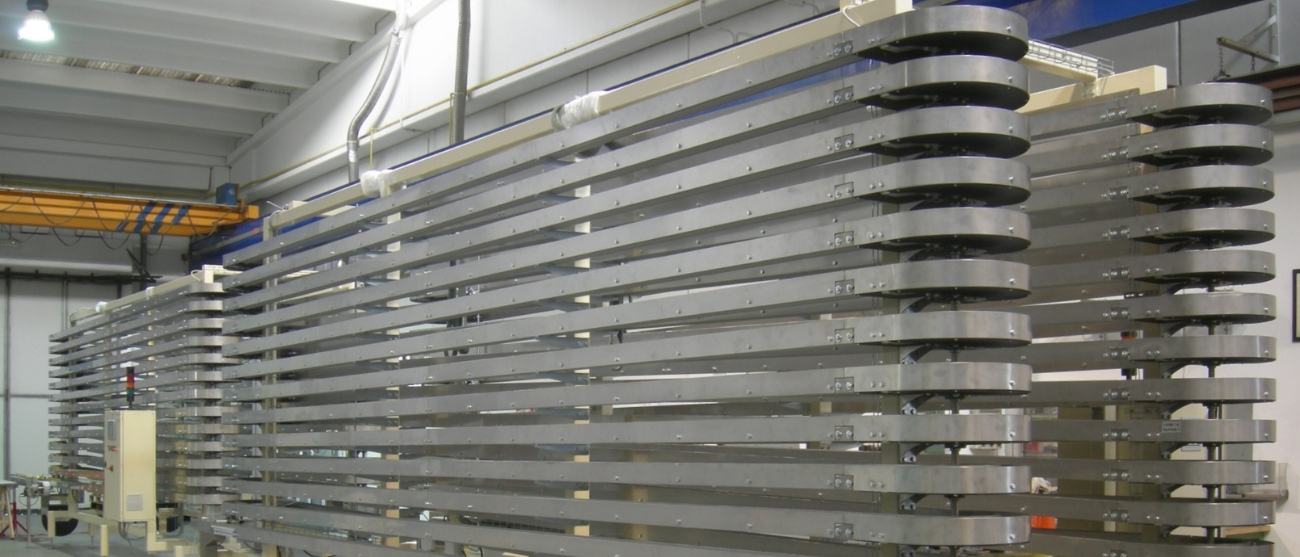
  • Spiral conveyors.

I want to focus on spiral conveyors because, in these cases, I consider them a valid solution.

It’s no coincidence that at Cibus Tec 2023, we presented the SVn-Bare lightweight spiral in collaboration with Ambaflex, specifically designed for agile aerial connections between primary and secondary packaging with significant economic advantage without compromising on quality and achievable peak speeds.

Another “powerful weapon” to improve the efficiency of packaging lines is represented by buffer systems; at MH, we can’t talk about them enough because they can really make a difference.

Buffer systems, for example, allow for:

  • Compensating for operational differences between two machines connected in series;
  • Regularizing the flow and preventing the processing line from constantly stopping;
  • Recovering productivity in the event of micro-stops on downstream machines.

However, integrating a buffer system at a later stage into an existing line is not straightforward; this operation requires significant attention and a series of specific evaluations regarding the performance outcomes to be achieved.

Adaptations to environmentally friendly packaging.

Another highly topical issue leading companies to plan a series of investments to modify their packaging lines is the need to adapt to the use of low-environmental-impact packaging.

When I talk about “low-environmental-impact packaging,” numerous possibilities open up that include solutions aimed at reducing packaging material or actually replacing plastic with paper, cardboard, or compostable material.

In these cases, the packaging process must keep up with progress. And keep in mind that companies will increasingly have to deal with changes imposed by a search for sustainability in processes.

To this end, at M.H., we are continuously investing in research and development of products capable of offering customers innovative and sustainable solutions in line with new market needs and regulatory requirements.

For example, the Sani-Flex hygienic design transport system, our standard for the transport of naked products, is specifically designed to meet stricter regulations; Saniflex takes into account the sanitization needs of some products to help reduce bacterial load during the process.

Another example is our partnership with Intralox for the construction or development of special products such as spiral elevators, ThermoDrive belts, and passive ARB conveyors.

These mentioned are just some of the solutions designed by M.H. to support companies in the process of modernizing their packaging lines.

If you also need to make your lines more functional and efficient, do not hesitate to contact us; we will guide you on a path to optimizing productivity specifically tailored to your needs.
Crackers, rusks and biscuits are goods that require particular care and are always packaged in a stack, one on top of the other.
Because of their form and the method of primary packaging, they require special conveyor systems.

To meet this specific need, in the phase after cooling that usually takes place on wide conveyor belts, we at M.H. Material Handling have developed a dedicated line of conveyors with a modular plastic chain system, FDA certified for use in the food industry.

Compared to traditional belt systems, this solution offers significant benefits in terms of ease of use and maintenance.

Our decade of experience has taught us how much demand there is for systems that can be easily adapted to align with companies’ packaging process and to optimise their productivity.

Let’s start with a premise: buffer systems can make a difference to the line’s efficiency.
The choice of model depends on various considerations (including financial ones) but there are three variables that must be kept in mind.

It is only by carefully considering these factors that we can move to a rapid consideration of the investment in the purchase of a buffer.

With MH Buffer Systems, you will no longer have to worry about inefficiencies. Take advantage of our expertise and technology to become a reference for efficiency in your sector.

When a company needs to install a merge conveyor, there are a range of variables that make the decision a difficult one.

The need for a merge conveyor in a packaging line is itself enough to indicate a process with a very high degree of complexity and automation throughout.

Choosing the right merge conveyor means taking into account:

  • how it protects the quality of the items;
  • making sure the machines downstream work as intended;
  • the efficiency of the entire packaging line.

It is clear therefore that mistakes could be critical.
The risk of ending up with an ineffective and obsolete packaging line is too high. That is why, whenever a client asks me which model is the best fit, I always start with a thorough analysis of their current operations, needs and expectations.

So, let’s start with a quick overview of these machines, explaining their purpose, their benefits and their limitations.

To start with, there are different types of merge conveyors, but the majority fall into one of two broad categories: mechanical (or buffer) merges and dynamic merges.

Buffer merges

This product is equipped with “gates” at the entry lanes that remain closed until the convergence area is free, at which point they let the items through one after the other.

This is a simple and cost-effective solution that works as long as two conditions are met:

  • the items must be able to withstand the pressure during the buffering phase;
  • the downstream machines must be able to receive the items in a convoy without being triggered to do so.

The first point is related to the integrity of the items, and essentially means that it is appropriate only for boxes, trays and products stacked in tight packaging.

The second point requires greater detail.
As they leave the merge, the items are touching each other, or very close to it, but the speed of the conveyor belt is the same as it would be with products that space out the items with one item’s worth of space between one and the next.
The average productivity of the line doesn’t change, but when the convoy arrives downstream, the machine’s productivity at that moment is doubled.

That is why the machine must be able to manage the flow, otherwise it is necessary to regulate the flow with one conveyor belt to increase the speed and another to decrease it after the merge; however, this solution is naturally bulkier, with two more motors and a more complicated logic controller.

Dynamic merges

When handling items that cannot be buffered for fear of overlap (generally pillow pouch or flowpack packaging) or damage caused by excessive pressure or because downstream machines need the items to arrive at a regular frequency and with a certain distance between one item and the next, then it becomes necessary to install a dynamic system.

A dynamic belt merge is a scalable system consisting of a series of modulating conveyor belts that increase or decrease the speed of the items as they come through, ensuring enough space to avoid a situation where two items reach the convergence point at the same time.

With these devices, the products are always handled one at a time, thereby avoiding having groups of items together and ensuring regular spacing. As the production pace increases, the number of modulators must also increase.

M.H. is an Italian brand with thirty years of experience with handling movement and logistics within production facilities in every sector of industry, with a range of solutions for buffer systems.

When it comes to dynamic merge conveyors, MH’s fastest system isthe HP dynamic system that can reach manufacturing of up to 600 ppm for 150mm flowpacks. Depending on the weight and packaging of the items, it is possible to use up to five phases of conveyors with brushless DC motor and vacuum suction to manage rapid acceleration.

Our wealth of experience means that M.H. is also able to support companies in optimising and streamlining their packaging lines with our innovative and technologically advanced solutions.

he first questions that we have to ask ourselves in these situations are: Are my packaging machines suited to this system? Can my goods be conveyed using this type of merge?


Buffer or mechanical merges are equipped with “gates” at the entry lanes that remain closed until the convergence area is free; once the gates have been opened, these release the products through one after the other.

If you want to find out more about our products or to discover how you can optimise your packaging process

It is necessary to insert a belt merge, which indicates that we’re working with a packaging line with a high degree of complexity and automation.
Process optimization is the goal, improving the packaging machine’s performance. But if you install the “wrong” system, you risk the opposite effect of having to contend with regular unplanned downtime.

When it comes to dynamic belt merges, we at MH have developed the HP dynamic system that can reach manufacturing of 600 ppm for 150mm flowpacks.


This system includes one-by-one timing of the items, created using a multi-belt system with independent power for each of the entry lanes. The machine’s control system enables oversight of the step between the packaging coming out of the system and ensures that the timing occurs without contact, removing the risk of jams, overlaps or damage.

Those who work with baked goods on a daily basis know all too well the critical importance of the packaging step.

Mistakes are not an option, and can lead to problems on the packaging line, compromising the integrity of the products and jeopardising the hard work done in preparing them.

All of these can lead to unplanned production downtime which, as you will know, potentially creates delays, problems and significant financial consequences.

Let’s begin by accepting the premise that often, especially in our country,food producers have two vital needs:

  • maximising space, as the available surface area reserved for production — and especially packaging — is limited and precious;
  • streamlining the packaging process as much as possible.

Taking these considerations into account, it is clear that conveyor belts have a vital role to play in packaging. The right conveyor belt can make all the difference.

So, let’s take a look at the different types of conveyor belts and when we might use them, taking into account that with baked goods it is worth distinguishing between different categories of products.

Regarding the cooling method, it can either be natural, in water (immersion or spray) or in a controlled environment (with dozens of different technological solutions available). The conveyor belts that make up the cooling system can be either spiral belts (adapted to reduce the necessary space for the cooling system), large conveyor belts or conveyors for baking trays.

Bread and dough products

When we talk about bread and dough products, they can take countless different forms: it goes without saying that each form has its own “rules” for conveying and packaging.

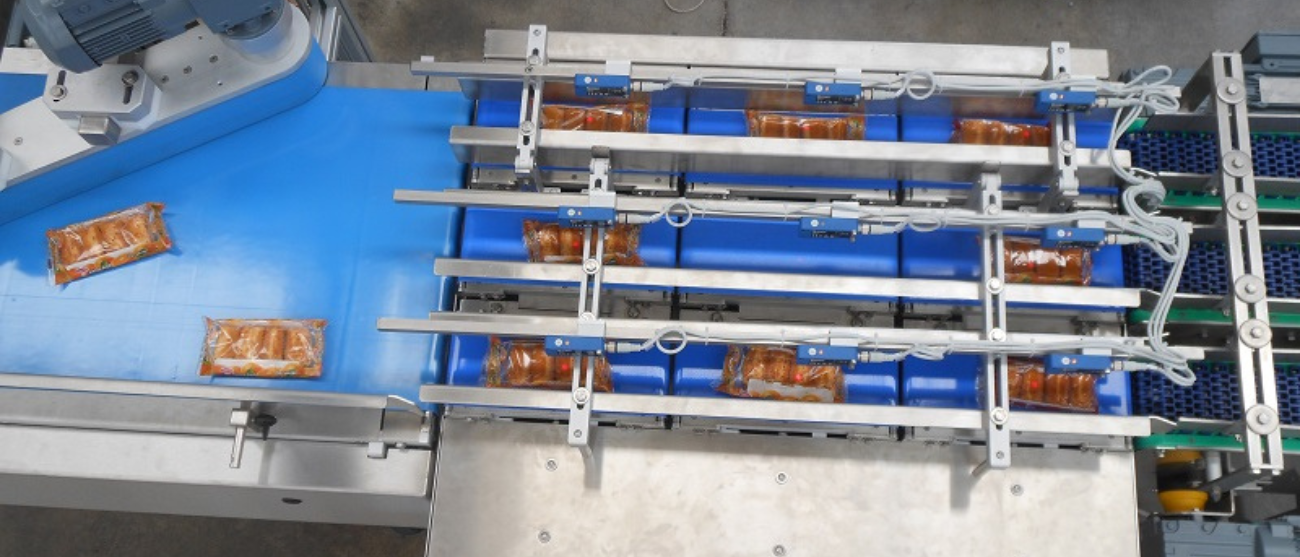
A recurring process requires a cooling system with a spiral conveyor followed by chicane aligners downstream that feed into the primary packaging machine.

The aligner consists of a series of wide belts with increasing speed, equipped with bulkheads and motorised diverters that channel the items through a series of chicanes that carry them through one or more neat lines.

The packaging machines could be either horizontal flowpacks, or vertical in the case of mini bread rolls, for example.

With Pullman sandwich loaves, the loaves pass through slicing machines that slice the bread before it’s packaged.

Bread in its various different forms very rarely comes in secondary packaging. It would far more commonly be placed directly in cardboard boxes or crates (depending on whether it is destined for large-scale retail or HoReCa). Here, merges and item layering systems may be useful, as they can naturally be buffered “with pressure”.

Crackers, rusks and biscuits

These goods require particular care and are always packaged in a stack, one on top of the other.

They therefore require special conveyor systems.

To meet this need, in the phase after cooling that usually takes place on wide conveyor belts, M.H. Material Handling has developed a dedicated line of FDA-certified conveyors with a modular plastic chain system for use in the food industry.

This solution offers significant benefits in terms of ease of use and maintenance compared to traditional belt systems. Thanks to its modular design, this type of belt guarantees extensive flexibility in designing the layout of the conveyor belts.

After this step, the goods are ready to be loaded as “packs” into the horizontal flowpack or wrapping machine.

Shortbread

As above, here too the cooling takes place on broad conveyor belts, but downstream the system that funnels the goods into the packaging machines varies greatly depending on the type of packaging required.

If the shortbread is individually packaged, they will have to be stacked one on top of the other; here too conveyor belts with a modular plastic chain offer the ideal solution.

However, if the shortbread is packaged in bags, the packaging machines funnel them in from above. Here we would recommend special conveyor belts that place the shortbread one on top of the other; there are then lift conveyor belts that load the shortbread onto weighing machines above the packaging machines.

Lift conveyor systems with modular chains are highly reliable and far easier to use and maintain than traditional bucket lift systems. They are ideal for continuous feeding of overhead lines[p1] , vertical packaging machines and multi-head weighing machines.

Cakes and pastries

Typical patisserie products, of the kind you might have for breakfast, are more durable than you might think.
They are cooled on spiral conveyors and packaged in horizontal flowpacks (as with bread, except with mini goods that are packaged vertically) and loaded using aligners.

These categories of goods are by far the most common within this sector; with certain exceptions, such as breadsticks, that have their own dedicated packaging lines.

Another scenario is that of frozen baked goods, as the presence of a constant level of humidity in the packaging line requires stainless steel conveyor belts that are resistant to corrosion and can be washed down.

As this brief overview has hopefully demonstrated, there are many factors to take into consideration and each category of baked goods has its own requirements. To complicate matters further, the precise specifications of the packaging machine impact the type of conveyors that work with them.

To optimise the packaging process of baked goods, you must be confident that the conveyor belts in use offer technologically advanced solutions that are also compatible with the packaging machines in the line.

M.H. is an Italian brand with thirty years of experience with handling movement and logistics within production facilities in every sector of industry, providing conveyor belts, merge and sort buffer systems, item rotators and flippers, lifts, destackers and other accessories necessary in the packaging and product manufacturing process.
Thanks to their modular design, M.H.’s products are interchangeable and easy to integrate into existing lines.

To find out more about how to improve the efficiency of the entire packaging process of your products, GET IN TOUCH TO DISCUSS.

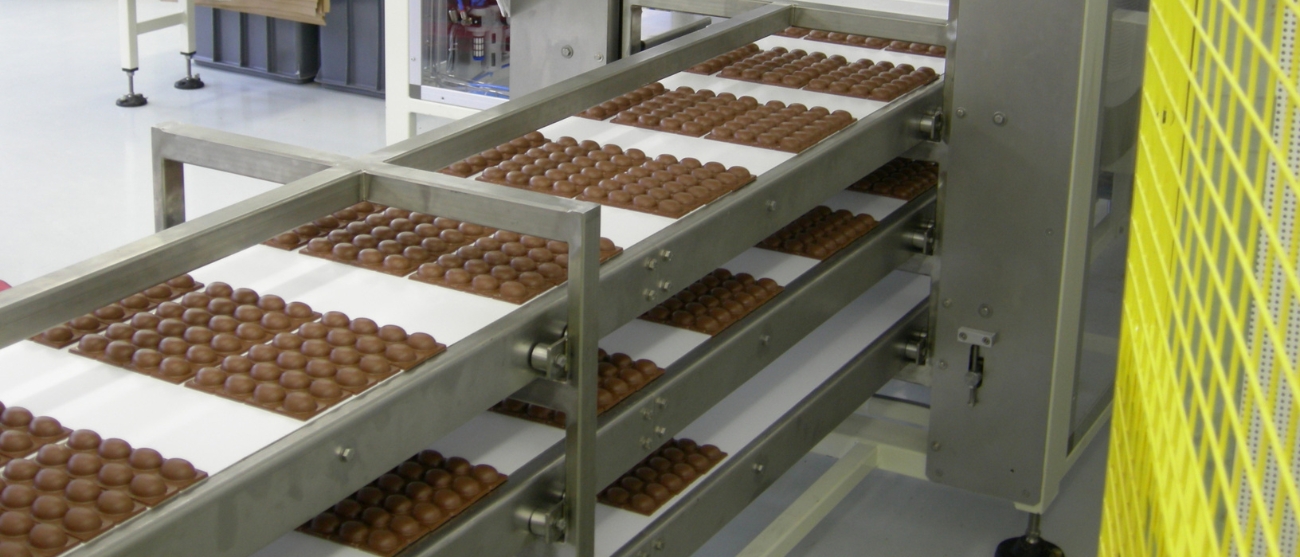
Those whose business involves chocolate (in all its many forms) know all too well the importance of the stage in which the “moulded” products are transferred to the primary packaging machine.

This is the moment in which a series of variables enter the picture, tied to the form of the product and the feeding system of the packaging machine. Added to this is a problem of available space: production facilities are not always overly generous with space to dedicate to packaging.

Bearing this in mind, it is not hard to see how important it is to have an ad hoc conveyor system that takes into account:

  • the type of product to be transported;
  • the feeding system of the primary packaging machine;
  • available space;
  • any devices that may be able to increase the efficiency of the line.

That is why, in this blog post I would like to provide an overview of the main feeding systems for primary packaging of chocolate.

All products, from the classic chocolate bars, through “hollow” forms (such as Easter eggs and bunnies, for example), all the way to the most carefully crafted pralines share a fundamentally similar production process, known as moulding. This is the most fascinating moment in the process, the one in which the chocolate takes shape.

Moulding generally involves the products travelling through special moulds and trays, so there are no particular differences between one product and the next in terms of the conveyor technology required.

When the chocolate is removed from the moulds (known in jargon as “demoulding”) the differences begin to be felt between the different types of products and packaging.

There are essentially three types of feeding system.

Hollow eggs and delicate/intricate pralines

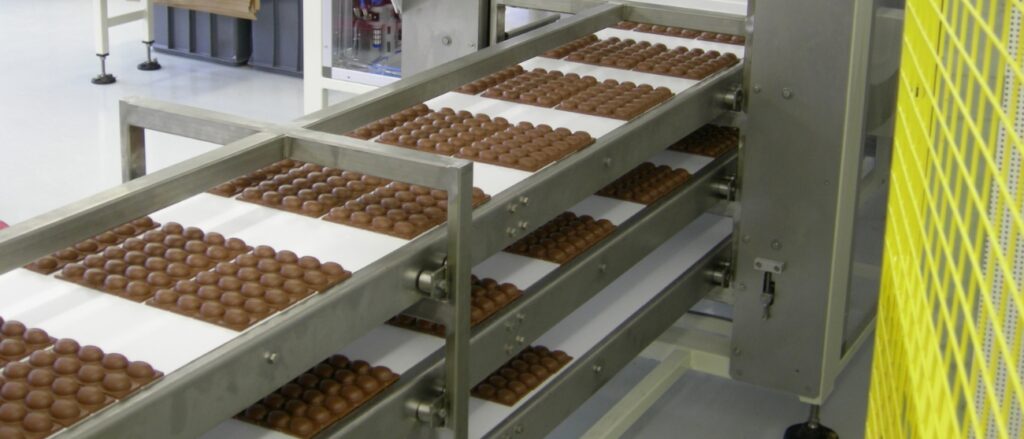
In these cases, the product remains in trays known as counterplates until the moment they are loaded into the packaging machine, usually using a so-called “pick and place” system.

This process generally involves the following equipment:

  • Conveyor belts

These can be of different types and they carry the plates either along the short or long sides, facing forwards.

  • Expulsion system

Placed after the metal detector and activated by pneumatic cylinders or brushless motors, this is responsible for ejecting plates with contaminated products. The plates must then be cleaned and reinserted manually (in the majority of cases).
Only lines that handle products with high margins can justify a fully automated recovery system.

  • Elevators

Bucket or ledge elevators are the ideal solutions for lines with relatively long work cycles. The ideal solution incorporates a motorised brushless axis to control the positioning and acceleration, offering a solution that ensures fluid and risk-free motion even when the plates are full.

  • Buffer

For these types of products, the natural choice is LIFO buffer systems (Last In — First Out) such as Pater Noster

  • Plate rotator

This device is usually the last one in the return line. The plate is presumed empty, but the packaging loader may have missed a few pieces that are still in the mould; therefore, before returning it to the demoulding position, it must be turned upside down and shaken to ensure any residual pieces fall out.
Once the plate has been definitively emptied, it can return to the start of the line and restart the cycle.

Small flat-bottomed chocolates

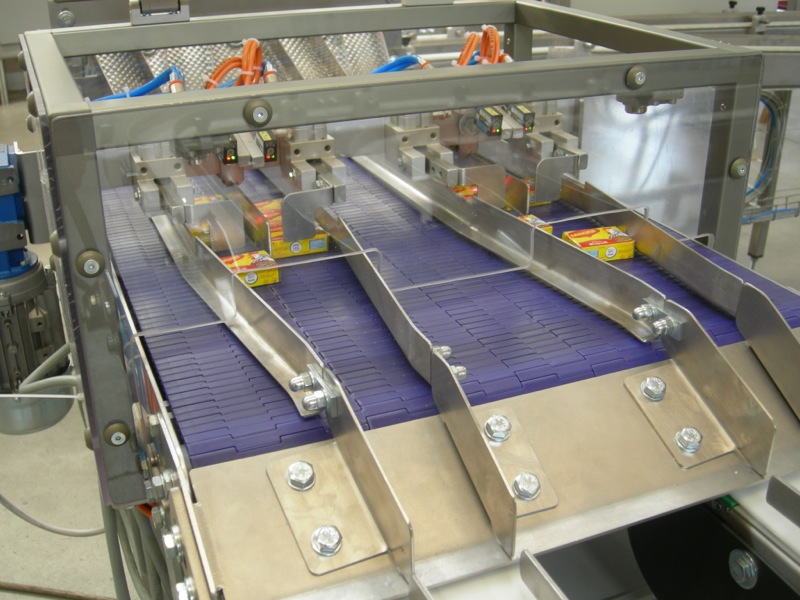
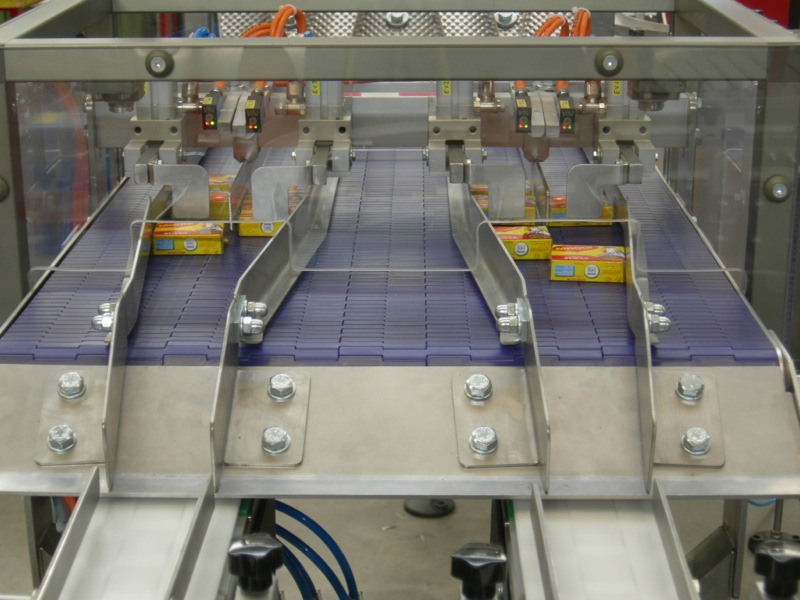
These usually use chicane conveyor belts that align the product and divert it towards the different wrappers.

Chocolate bars

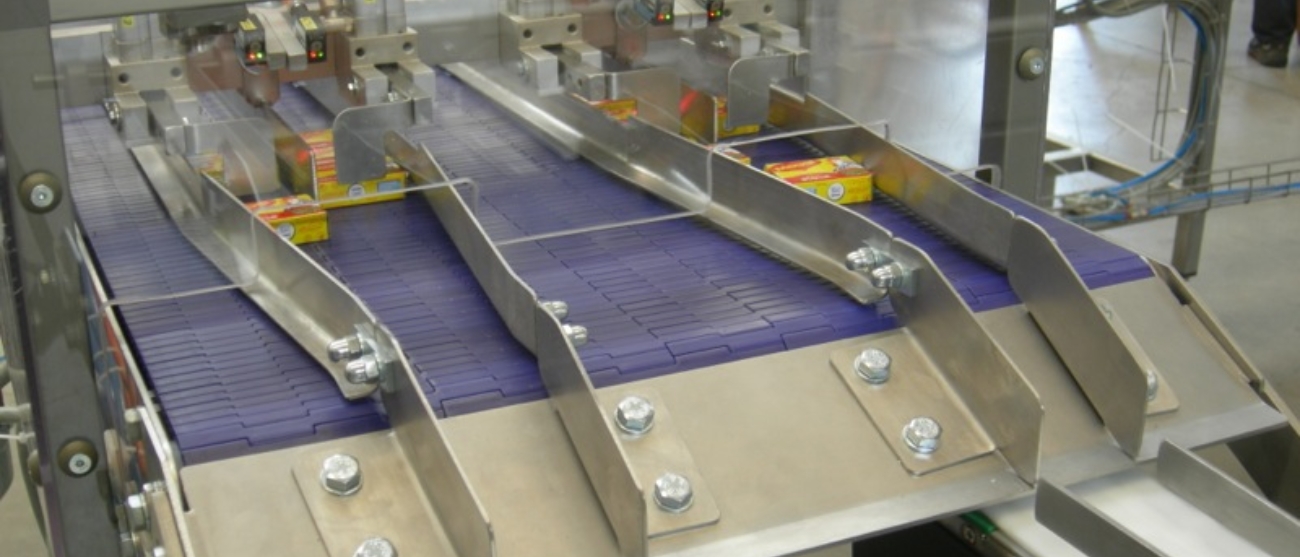
This uses the classic rank feeding system that can load both wrapping paper and flowpack. In these cases, the products must be arranged in single file at one or more exits before they enter the machine.

To meet this need, merge and align groups for unpackaged products are used.

The standard merge group consists of three belt or modular chain conveyors that operate at different speeds, to separate the arriving products. Above the belts there are a few pairs of fixed guides or motorised belt diverters with adjustable inclines, that slow some products down and allow those they do not touch to pass, thereby breaking up the threading process.

To buffer large volumes of the unpackaged product by rank, we need a multiple cleave belt that follows the FIFO principle (First In — First Out); the cleaves can either be fixed, fed by a tilting conveyor or organised in a single rack that can be raised and lowered. This second solution is critical in production facilities where available space is at a premium.

The packaging machines are fed by exit lines that are perpendicular to the primary transportation line. The exit lanes receive the product from the primary transportation line through oscillating devices.

Before they can reach the primary packaging, the products must often be rotated and separated to ensure the efficiency of the line. The task is carried out using a series of conveyor belts that carry out successive jumps in speed, to ensure adequate spacing between the products.

M.H. produces all of the solutions described above, focusing first and foremost on the specific needs of each client, to tailor and optimise the entire packaging process for them.

M.H. is an Italian brand with thirty years of experience with handling movement and logistics within production facilities in every sector of industry, providing conveyor belts, merge and sort accumulation systems, item rotators and flippers, lifts, destackers and other accessories necessary in the packaging and product manufacturing process.
Thanks to their modular design, M.H.’s products are interchangeable and easy to integrate into existing lines.

Improve the efficiency of your packaging line with our MH Scan Solution

Throughout my career, I have often come across companies who make the mistake of underestimating the importance of the packaging line of their products dei loro prodotti.

The result: Reduced efficiency and the risk that machines may not work at maximum capacity, or worse still, grind to a halt.

These situations happen because someone erroneously thinks that product packaging requires buying the primary and, if necessary, secondary packaging machines and nothing more, failing to take into account the systems necessary to connect them.

There is an image that often comes to mind when I have to tackle this kind of problem: I think of the conveyor belts like the circulatory system that carries blood around the body and allows the different organs to function. Different packaging machines have to be connected to each other by an efficient “circulatory system” that is able to iron out any discrepancies that may exist between them.

Underestimating the importance of this “circulatory system” can result in production problems and delays.

When would we need a storage system?

There are two situations in which storage systems are critical:

  • when we need to compensate for operating differences between two machines that are connected in series;
  • when we need to regain productivity during micro-stops of downstream machines.

The first condition typically occurs when an intermittent machine is connected to a continuous one; for example, when an upstream machine produces product groups at regular intervals, while the downstream machine requires an ongoing flow of products equidistant from each other.

In the second case, on the other hand, we have start-ups and shut-downs of two machines that are incompatible with each other.

In these cases a buffer is a simple solution that requires a few metres of conveyor belt to regulate the flow and avoid regular stoppages in the production process.

As you can imagine, the efficiency gains are significant.

Which buffer to choose?

The choice of system depends on various considerations (including financial ones) but there are three variables that must be kept in mind:

  • the operating method of the storage system;
  • the available storage space;
  • the recovery capacity.

It is only by carefully considering these factors that we can move to a rapid consideration of the investment in the purchase of a buffer.

How the buffer works

The buffer can either be LIFO(Last In First Out), in which, as the name suggests, the first product to enter the buffer is the last one to leave it, or FIFO (First In First Out), in which the first product into the buffer is the first one out.

Among FIFO systems, there is a choice of:

  • machines that are external to the production line;
  • machinery that keeps the product within the production line, gradually increasing the available transportation space. In the latter case, the product is fully traceable, and it is considered more of an advanced storage system rather than a buffer.

LIFO buffers are the cheaper and simpler models. They are particularly suited to non-perishable, with long expiry dates, that can wait a long time for final packaging.

FIFO systems, on the other hand, are recommended for fresh products that must pass through the packaging line within a limited time frame in order to retain their freshness. These machines are usually more complex and their price is often not far off that of the packaging machines themselves.

Storage space

The decision regarding the dimensions of the storage space is linked to the efficiency of the upstream and downstream packaging machines and the time it takes to bring them back online in cases of micro-stops. In cases of a longer stop caused by mechanical failure, it is unlikely that a system within the packaging line will be sufficient to avoid any interruption at all.

In most cases, the storage space can correspond to a production time of 2-5 minutes; obviously there may be situations in which the demand for storage is notably higher and in this case it is worth considering the cost-benefit analysis and the impact that the buffer’s presence might have on the time it takes to bring the packaging line back online.

Often, the long time to recover from a micro-stop is because the operator is unable to focus exclusively on fixing the problem, because the upstream products continue to arrive, with the potential for pressure and chaos along the line.
Real-world conditions have shown that the presence of a buffer can help to contain machine downtimes.

Another example might be whereproducts travel a long distance along the packaging line and the client wants the ability to fully empty them. In this case, the necessary space can rise to 20 minutes or more. Such situations are rare but can happen.

Recovery capacity

A properly sized packaging line requires a buffer that is able to recover the product during regular production. The downstream machine must also be able to work at a rate greater than its nominal one, usually 10%-20% faster.

The time for emptying the buffer depends on this recovery capacity.

For more information on this subject, I have published a video dedicated to choosing the right storage system.

M.H. is an Italian brand with thirty years of experience with handling movement and logistics within production facilities in every sector of industry. We offer dedicated solutions for LIFO and FIFO storage systems, tailored to the client’s needs.

Our wealth of experience and our innovative and technologically advanced solutions mean that M.H. is also able to support companies in optimizing and streamlining their packaging lines.

Insights, ideas and news
about product handling

A divider distributes a product flow across multiple outlets along a packaging line. One of the most common situations arises when an upstream machine has a higher capacity than the downstream machines and the flow needs to be split into multiple lanes. This is typical of high-speed and flowpack lines, at the transition from primary to secondary packaging. We have been working in this field for over forty years, across the food, beverage, pharmaceutical and packaging sectors.

On these lines, the main parameters are line speed and cadence. Beyond a certain output rate, even the fastest secondary packaging machines cannot keep up. This is the same limitation encountered with mergers.

Splitting the flow into multiple lanes also helps ensure machine reliability and durability over time. Downstream, this may mean using several product arranging units or a single pick-and-place machine operating on multiple lanes simultaneously.

Diverter or sorter? Understanding the differences

The term divider, however, covers different types of equipment. The most immediate distinction is between a diverter and a sorter.

A diverter sends identical products into different lanes without changing how the products themselves are handled.

A sorter, by contrast, can also separate products according to specific criteria. Different boxes are directed to different outlets and are not treated identically, because a particular code or product is routed to its designated outlet. From a design standpoint, a sorter consists of a straight conveyor section with lateral outlets.

The 7 parameters that influence the choice

Deciding whether you need a diverter or a sorter is only the starting point. Before comparing technologies, it is worth establishing the following:

  1. the nature of the product: its shape, stability, fragility and deformability,
  2. line speed,
  3. cadence,
  4. the number of outlets required,
  5. whether the product can be touched,
  6. whether it can withstand pressure,
  7. product dimensions.

The most common solutions and when to use them

The deciding factor is the number of outlets. The selection criteria change significantly between a one-to-two divider and a multi-lane system.

Multi-lane systems require at least a channel-system divider, suitable for products that can come into contact with one another. Because contact is permitted, the divider does not space the products at set intervals: instead, it stops them in the channel, allows them to accumulate, and then switches channels. A multi-channel solution can still be considered for fragile products, but only when it is absolutely certain that the preceding product has cleared the channel.

In multi-lane flowpack systems, we use a sequence of one-to-two dividers. The application becomes more complex when products are fragile or low-profile, with a risk of overlapping.

A flap divider moves the product by making contact with it, provided the product can tolerate this. It is limited to two outlets: to obtain more, several finger-type dividers are generally arranged in a cascade. This is the simplest and therefore least expensive solution. Essentially, it consists of a deflecting paddle, with the limitations described above.

The soft touch system guides the product gently and is used on flowpack lines where accumulation is not possible. This solution also normally operates with one inlet and two outlets.

For robust, stable products such as cartons, boxes or trays, a mechanical multi-lane divider is a good solution, directing the flow by means of pallets, mobile channels or drawers.

Special solutions and when they make sense

Magic Sorter

When a product is very flat, thin or deformable, side guides can become a problem. The product may slip between the guide and the conveyor surface and become jammed.

In these cases, M.H. uses the Magic Sorter as either a divider or a merger. Product movement is controlled by a modular chain with embedded balls, suitable for items that cannot be handled using conventional side guides.

The Magic Sorter also makes it possible to create multiple outlets with the same system. This flexibility does, however, come with a throughput limitation: in the fastest applications, it can handle approximately 120 pieces per minute, which is lower than the throughput achievable with other sorting technologies.

AIM

AIM combines a modular conveyor belt with a pneumatically actuated, recessed pusher. The system acts on the lower part of the product, moving it through contact with its side. It is therefore suitable for non-deformable items that can withstand lateral contact.

Its main advantage is washdown suitability. The pneumatic actuation system withstands frequent washing, particularly when a dedicated stainless-steel cylinder is used. AIM can achieve an indicative maximum throughput of 120 pieces per minute.

Like the Magic Sorter, AIM is not used on flowpack lines: the small size of the products prevents the balls or the pusher from controlling them properly. In this case, the limitation is related to product dimensions, not line throughput.

ARB

ARB is a solution intended exclusively for end-of-line applications, where larger products such as boxes and other packages ready for subsequent processing stages are handled. One of its most common applications is feeding palletisers.

Product size alone is not enough to determine whether it can be used. The contact surface must also be checked: the bottom of the product must be even. This technology therefore requires specific conditions and differs from the dividers used between primary and secondary packaging.

Cost is another factor in the decision. ARB requires a higher investment and would not be justified where a simpler solution can perform the same task. It is therefore considered when the product type and end-of-line application genuinely warrant its use.

How to choose the right divider

Once these points have been clarified, the most suitable technology becomes much easier to identify.

Without this analysis, there is a risk of choosing a divider based on throughput alone, overlooking product characteristics, pressure resistance and the operating environment.

At M.H. Material Handling, we design and integrate all these solutions, from mechanical multi-lane dividers and the Magic Sorter to Intralox ARB and AIM applications. We support our customers in analysing product flows and selecting the most suitable configuration.

If divider selection is still an unresolved aspect of your project, we can assess it together, considering the product, throughput and required destinations to identify the best solution.

How many types of conveyors are there, and how do you choose the most suitable one for a specific application?

In this episode of ConveyorU Academy, our mascot Convy asks Luca Fontana, CEO of M.H. Material Handling, who walks us through the main conveyor technologies available and the key factors to consider when making the right choice.

The most suitable conveyor depends on the type of product, the stage of the production process, and the characteristics of the line.

That’s why there is no single best technology for every application: it’s essential to find the right balance between different requirements, such as safety, speed, and the characteristics of the product being handled.

Want to improve your production line’s efficiency? Contact us and request a no-obligation MH Scan Solution consultation. We’ll help you analyze your application, identify potential issues, and develop a solution tailored to the actual needs of your facility.

Chocolate is irresistible. Less so when it ends up sticking to the conveyor belts on your production line.

In the chocolate and confectionery industry, sugar-based residues can make conveyor cleaning particularly challenging, especially when products move through multiple processing stages before reaching the packaging area.

At M.H., in collaboration with Steam Italy, we have developed a cleaning system designed for different conveyor configurations, from continuous-surface monolithic belts to modular plastic chains.

Different conveyor types come with different characteristics and cleaning requirements, which means they also require different cleaning approaches.

Do you have a specific cleaning challenge on your production line? Contact us: we can assess your conveyor configuration together and identify the most suitable solution.

A high-quality packaging line can deliver reliable performance for decades, especially when supported by careful engineering and proper maintenance.

The service life of a system represents significant value, but being fully operational does not always mean it can meet today’s production, technological and regulatory requirements.

New packaging materials, sustainability goals, and increasingly demanding industry standards require systems capable of evolving – a particularly important consideration in the food industry, where hygiene, ease of cleaning, and safety are fundamental requirements.

Do you want to learn how to adapt your system to new regulations and changing production requirments?

Contact us for a technical consultation.

Converging multiple product lanes into a smaller number of lanes may seem like a simple operation. In reality, the way products are collected, timed and delivered to the downstream machine can have a significant impact on the consistency of the entire process.

This is why designing a lane merger is not simply a matter of considering line speed. First of all, it is necessary to understand how the product behaves: its shape, stability, fragility, ability to run in contact with other products, and the pitch required by the downstream machine are all factors that help define the right solution.

Based on these parameters, M.H. Material Handling designs the merging configuration best suited to the characteristics of the line and the product.

The first criterion is the product: can it withstand accumulation?

Even before speed is considered, the assessment starts with the product and its ability to withstand accumulation.

A product that can tolerate accumulation can withstand the pressure generated by products touching and pushing against one another. Boxes, trays and products stacked in tightly packed formats fall into this category.

A fragile product, or one prone to overlapping, cannot withstand this type of stress, and a pressure-based system could compromise its integrity.

This is why resistance to accumulation is the first factor to be assessed, as it determines whether a pneumatic or dynamic lane merger is required even before line throughput is considered.

There is, however, one useful exception to bear in mind.

Even with a product that can withstand accumulation, the presence of many formats with significantly different widths often makes a dynamic solution preferable. This avoids format changeovers using adjustable or automatically controlled guides and, because the products do not come into contact with one another, eliminates the risk of misalignment.

Pneumatic, DU Series or HP Series: the right technology for each product

A pneumatic lane merger is the simplest and most cost-effective solution, but it is suitable only for products that can tolerate accumulation.

It operates using gates on the infeed lanes, which release the product rows in sequence, and requires two conditions: the products must be able to withstand pressure during accumulation, and the downstream machine must be capable of receiving products in a continuous train without being adversely affected.

The second requirement has a specific technical reason. At the outlet, the products are close together or touching. When this train reaches the downstream machine, the instantaneous speed seen by the machine is therefore twice the average speed. Either the downstream equipment must be able to handle this, or the flow must be normalised using a deceleration conveyor followed by an acceleration conveyor, at the cost of a larger footprint, two additional motors and more complex control logic.

The pneumatic solution is also well suited to a particular application: where the carton itself is the primary package, as is common in the pasta industry, in the section between secondary packaging and the case packer, where the product can be accumulated.

When, on the other hand, the product is delicate or must be handled without contact, dynamic lane mergers are used. M.H. offers two series.

The DU Series merges products by reducing the number of lanes through anti-overlap timing belts operating at controlled differential speeds, one for each infeed lane. Products are handled individually and without contact, making the system suitable for fragile products or products prone to overlapping, at speeds of up to approximately 240 pieces per minute.

The HP Series is the evolution of the DU Series, developed specifically for high-speed flow-wrapping lines and for connections between primary and secondary packaging. In this case, pressure is completely eliminated because the products must never come into contact. Each item is individually timed by means of a multi-belt system with independent brushless drives for every infeed lane, combined with blower-generated vacuum for higher acceleration rates, reaching up to 600 pieces per minute at the outlet. In flow-wrapping applications, precise product timing is essentially mandatory, as it is the only way to prevent products from overlapping.

Outlet pitch: a detail that should not be underestimated

As speed increases, it becomes essential to achieve the most consistent possible product pitch at the outlet of the lane merger, because this determines how the downstream machine receives each item.

A product flow delivered in trains can push the downstream machine beyond its production limits because of the instantaneous speed peaks described above. Individual product timing, on the other hand, controls the distance between packs and transfers them without contact, reducing the risk of jams and overlaps.

The choice always starts with the product

In every case, the starting point is always the product. The first step is to determine whether it can withstand accumulation, then assess its fragility and shape, the required production rate and the number of lanes to be merged, and finally the type of downstream machine, particularly whether it is a flow wrapper positioned between primary and secondary packaging.

The right technology emerges from these answers: a pneumatic lane merger for products that can withstand pressure, the DU Series for products requiring contact-free handling, and the HP Series for high-speed flow-wrapping applications.

At M.H. Material Handling, we manufacture material-handling systems and efficiency solutions for packaging lines in the food industry and related sectors. Over more than forty years of field experience, from food & beverage to pharmaceuticals and packaging, we have developed the expertise required to identify where lane merging can make a real difference and where it is unnecessary. On this basis, we design customised pneumatic and dynamic lane mergers from the DU and HP Series, starting with an analysis of the production line.

If you are planning a new line or a revamping project and lane merging is still an open issue, we can assess it together to identify the most suitable configuration.

Is your packaging line inefficient? Just add a buffer and the problem is solved.

Or at least, that’s what many people think.

Adding a buffer to an existing line can turn into an expensive and unnecessary investment. Before proceeding with the installation, carefully assess all the preliminary factors: an in-depth analysis can help you avoid ending up with the same problems you started with.

To identify the most suitable solution for your packaging line, contact us: we’ll analyse your specific case and help you define the most effective solution.