M.H. – Material Handling

Luca Fontana

A divider distributes a product flow across multiple outlets along a packaging line. One of the most common situations arises when an upstream machine has a higher capacity than the downstream machines and the flow needs to be split into multiple lanes. This is typical of high-speed and flowpack lines, at the transition from primary to secondary packaging. We have been working in this field for over forty years, across the food, beverage, pharmaceutical and packaging sectors.

On these lines, the main parameters are line speed and cadence. Beyond a certain output rate, even the fastest secondary packaging machines cannot keep up. This is the same limitation encountered with mergers.

Splitting the flow into multiple lanes also helps ensure machine reliability and durability over time. Downstream, this may mean using several product arranging units or a single pick-and-place machine operating on multiple lanes simultaneously.

Diverter or sorter? Understanding the differences

The term divider, however, covers different types of equipment. The most immediate distinction is between a diverter and a sorter.

A diverter sends identical products into different lanes without changing how the products themselves are handled.

A sorter, by contrast, can also separate products according to specific criteria. Different boxes are directed to different outlets and are not treated identically, because a particular code or product is routed to its designated outlet. From a design standpoint, a sorter consists of a straight conveyor section with lateral outlets.

The 7 parameters that influence the choice

Deciding whether you need a diverter or a sorter is only the starting point. Before comparing technologies, it is worth establishing the following:

  1. the nature of the product: its shape, stability, fragility and deformability,
  2. line speed,
  3. cadence,
  4. the number of outlets required,
  5. whether the product can be touched,
  6. whether it can withstand pressure,
  7. product dimensions.

The most common solutions and when to use them

The deciding factor is the number of outlets. The selection criteria change significantly between a one-to-two divider and a multi-lane system.

Multi-lane systems require at least a channel-system divider, suitable for products that can come into contact with one another. Because contact is permitted, the divider does not space the products at set intervals: instead, it stops them in the channel, allows them to accumulate, and then switches channels. A multi-channel solution can still be considered for fragile products, but only when it is absolutely certain that the preceding product has cleared the channel.

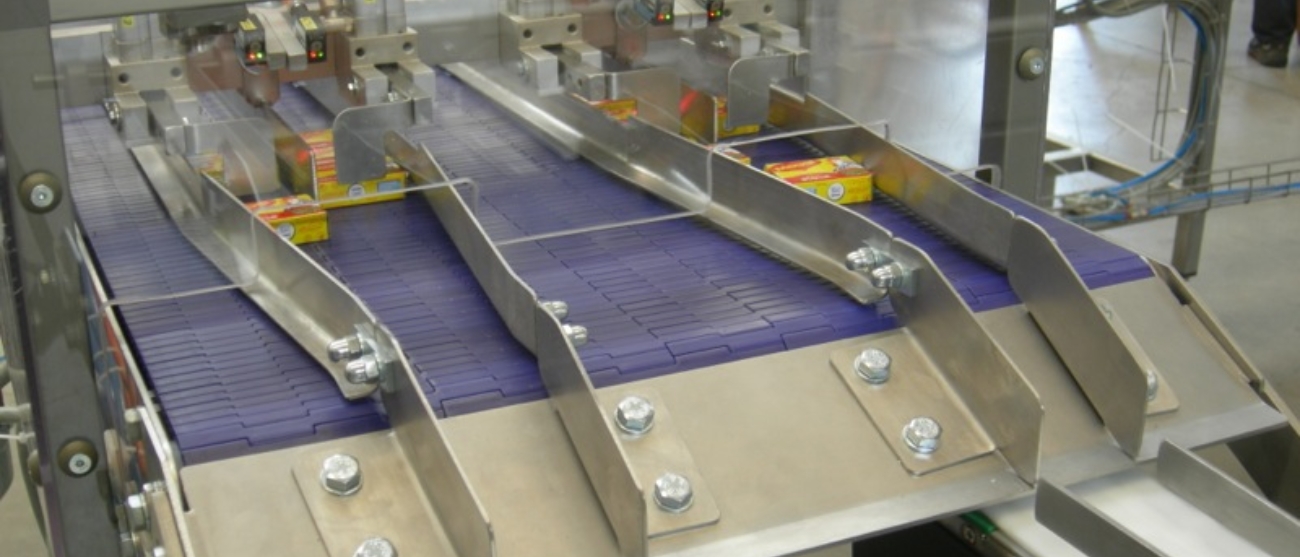
In multi-lane flowpack systems, we use a sequence of one-to-two dividers. The application becomes more complex when products are fragile or low-profile, with a risk of overlapping.

A flap divider moves the product by making contact with it, provided the product can tolerate this. It is limited to two outlets: to obtain more, several finger-type dividers are generally arranged in a cascade. This is the simplest and therefore least expensive solution. Essentially, it consists of a deflecting paddle, with the limitations described above.

The soft touch system guides the product gently and is used on flowpack lines where accumulation is not possible. This solution also normally operates with one inlet and two outlets.

For robust, stable products such as cartons, boxes or trays, a mechanical multi-lane divider is a good solution, directing the flow by means of pallets, mobile channels or drawers.

Special solutions and when they make sense

Magic Sorter

When a product is very flat, thin or deformable, side guides can become a problem. The product may slip between the guide and the conveyor surface and become jammed.

In these cases, M.H. uses the Magic Sorter as either a divider or a merger. Product movement is controlled by a modular chain with embedded balls, suitable for items that cannot be handled using conventional side guides.

The Magic Sorter also makes it possible to create multiple outlets with the same system. This flexibility does, however, come with a throughput limitation: in the fastest applications, it can handle approximately 120 pieces per minute, which is lower than the throughput achievable with other sorting technologies.

AIM

AIM combines a modular conveyor belt with a pneumatically actuated, recessed pusher. The system acts on the lower part of the product, moving it through contact with its side. It is therefore suitable for non-deformable items that can withstand lateral contact.

Its main advantage is washdown suitability. The pneumatic actuation system withstands frequent washing, particularly when a dedicated stainless-steel cylinder is used. AIM can achieve an indicative maximum throughput of 120 pieces per minute.

Like the Magic Sorter, AIM is not used on flowpack lines: the small size of the products prevents the balls or the pusher from controlling them properly. In this case, the limitation is related to product dimensions, not line throughput.

ARB

ARB is a solution intended exclusively for end-of-line applications, where larger products such as boxes and other packages ready for subsequent processing stages are handled. One of its most common applications is feeding palletisers.

Product size alone is not enough to determine whether it can be used. The contact surface must also be checked: the bottom of the product must be even. This technology therefore requires specific conditions and differs from the dividers used between primary and secondary packaging.

Cost is another factor in the decision. ARB requires a higher investment and would not be justified where a simpler solution can perform the same task. It is therefore considered when the product type and end-of-line application genuinely warrant its use.

How to choose the right divider

Once these points have been clarified, the most suitable technology becomes much easier to identify.

Without this analysis, there is a risk of choosing a divider based on throughput alone, overlooking product characteristics, pressure resistance and the operating environment.

At M.H. Material Handling, we design and integrate all these solutions, from mechanical multi-lane dividers and the Magic Sorter to Intralox ARB and AIM applications. We support our customers in analysing product flows and selecting the most suitable configuration.

If divider selection is still an unresolved aspect of your project, we can assess it together, considering the product, throughput and required destinations to identify the best solution.
How many types of conveyors are there, and how do you choose the most suitable one for a specific application?

In this episode of ConveyorU Academy, our mascot Convy asks Luca Fontana, CEO of M.H. Material Handling, who walks us through the main conveyor technologies available and the key factors to consider when making the right choice.

The most suitable conveyor depends on the type of product, the stage of the production process, and the characteristics of the line.

That’s why there is no single best technology for every application: it’s essential to find the right balance between different requirements, such as safety, speed, and the characteristics of the product being handled.

Want to improve your production line’s efficiency? Contact us and request a no-obligation MH Scan Solution consultation. We’ll help you analyze your application, identify potential issues, and develop a solution tailored to the actual needs of your facility.

Chocolate is irresistible. Less so when it ends up sticking to the conveyor belts on your production line.

In the chocolate and confectionery industry, sugar-based residues can make conveyor cleaning particularly challenging, especially when products move through multiple processing stages before reaching the packaging area.

At M.H., in collaboration with Steam Italy, we have developed a cleaning system designed for different conveyor configurations, from continuous-surface monolithic belts to modular plastic chains.

Different conveyor types come with different characteristics and cleaning requirements, which means they also require different cleaning approaches.

Do you have a specific cleaning challenge on your production line? Contact us: we can assess your conveyor configuration together and identify the most suitable solution.

A high-quality packaging line can deliver reliable performance for decades, especially when supported by careful engineering and proper maintenance.

The service life of a system represents significant value, but being fully operational does not always mean it can meet today’s production, technological and regulatory requirements.

New packaging materials, sustainability goals, and increasingly demanding industry standards require systems capable of evolving – a particularly important consideration in the food industry, where hygiene, ease of cleaning, and safety are fundamental requirements.

Do you want to learn how to adapt your system to new regulations and changing production requirments?

Contact us for a technical consultation.

Converging multiple product lanes into a smaller number of lanes may seem like a simple operation. In reality, the way products are collected, timed and delivered to the downstream machine can have a significant impact on the consistency of the entire process.

This is why designing a lane merger is not simply a matter of considering line speed. First of all, it is necessary to understand how the product behaves: its shape, stability, fragility, ability to run in contact with other products, and the pitch required by the downstream machine are all factors that help define the right solution.

Based on these parameters, M.H. Material Handling designs the merging configuration best suited to the characteristics of the line and the product.

The first criterion is the product: can it withstand accumulation?

Even before speed is considered, the assessment starts with the product and its ability to withstand accumulation.

A product that can tolerate accumulation can withstand the pressure generated by products touching and pushing against one another. Boxes, trays and products stacked in tightly packed formats fall into this category.

A fragile product, or one prone to overlapping, cannot withstand this type of stress, and a pressure-based system could compromise its integrity.

This is why resistance to accumulation is the first factor to be assessed, as it determines whether a pneumatic or dynamic lane merger is required even before line throughput is considered.

There is, however, one useful exception to bear in mind.

Even with a product that can withstand accumulation, the presence of many formats with significantly different widths often makes a dynamic solution preferable. This avoids format changeovers using adjustable or automatically controlled guides and, because the products do not come into contact with one another, eliminates the risk of misalignment.

Pneumatic, DU Series or HP Series: the right technology for each product

A pneumatic lane merger is the simplest and most cost-effective solution, but it is suitable only for products that can tolerate accumulation.

It operates using gates on the infeed lanes, which release the product rows in sequence, and requires two conditions: the products must be able to withstand pressure during accumulation, and the downstream machine must be capable of receiving products in a continuous train without being adversely affected.

The second requirement has a specific technical reason. At the outlet, the products are close together or touching. When this train reaches the downstream machine, the instantaneous speed seen by the machine is therefore twice the average speed. Either the downstream equipment must be able to handle this, or the flow must be normalised using a deceleration conveyor followed by an acceleration conveyor, at the cost of a larger footprint, two additional motors and more complex control logic.

The pneumatic solution is also well suited to a particular application: where the carton itself is the primary package, as is common in the pasta industry, in the section between secondary packaging and the case packer, where the product can be accumulated.

When, on the other hand, the product is delicate or must be handled without contact, dynamic lane mergers are used. M.H. offers two series.

The DU Series merges products by reducing the number of lanes through anti-overlap timing belts operating at controlled differential speeds, one for each infeed lane. Products are handled individually and without contact, making the system suitable for fragile products or products prone to overlapping, at speeds of up to approximately 240 pieces per minute.

The HP Series is the evolution of the DU Series, developed specifically for high-speed flow-wrapping lines and for connections between primary and secondary packaging. In this case, pressure is completely eliminated because the products must never come into contact. Each item is individually timed by means of a multi-belt system with independent brushless drives for every infeed lane, combined with blower-generated vacuum for higher acceleration rates, reaching up to 600 pieces per minute at the outlet. In flow-wrapping applications, precise product timing is essentially mandatory, as it is the only way to prevent products from overlapping.

Outlet pitch: a detail that should not be underestimated

As speed increases, it becomes essential to achieve the most consistent possible product pitch at the outlet of the lane merger, because this determines how the downstream machine receives each item.

A product flow delivered in trains can push the downstream machine beyond its production limits because of the instantaneous speed peaks described above. Individual product timing, on the other hand, controls the distance between packs and transfers them without contact, reducing the risk of jams and overlaps.

The choice always starts with the product

In every case, the starting point is always the product. The first step is to determine whether it can withstand accumulation, then assess its fragility and shape, the required production rate and the number of lanes to be merged, and finally the type of downstream machine, particularly whether it is a flow wrapper positioned between primary and secondary packaging.

The right technology emerges from these answers: a pneumatic lane merger for products that can withstand pressure, the DU Series for products requiring contact-free handling, and the HP Series for high-speed flow-wrapping applications.

At M.H. Material Handling, we manufacture material-handling systems and efficiency solutions for packaging lines in the food industry and related sectors. Over more than forty years of field experience, from food & beverage to pharmaceuticals and packaging, we have developed the expertise required to identify where lane merging can make a real difference and where it is unnecessary. On this basis, we design customised pneumatic and dynamic lane mergers from the DU and HP Series, starting with an analysis of the production line.

If you are planning a new line or a revamping project and lane merging is still an open issue, we can assess it together to identify the most suitable configuration.

Is your packaging line inefficient? Just add a buffer and the problem is solved.

Or at least, that’s what many people think.

Adding a buffer to an existing line can turn into an expensive and unnecessary investment. Before proceeding with the installation, carefully assess all the preliminary factors: an in-depth analysis can help you avoid ending up with the same problems you started with.

To identify the most suitable solution for your packaging line, contact us: we’ll analyse your specific case and help you define the most effective solution.

What happens when the connection between the machines in a packaging line is not designed correctly?

The risk is that slowdowns, accumulations, micro-stoppages and disruptions in the flow may occur, affecting the efficiency of the line and, over time, the overall performance of the plant.

This is the idea behind the new video series from ConveyorU, the M.H. Material Handling Academy dedicated to intelligent product handling in packaging lines.

Guiding you through this journey are Convy, the Academy’s mascot, who asks the questions of those who work in production plants every day, and Luca Fontana, CEO of M.H. Material Handling, who answers based on forty years of experience in line design.

In this first episode, they address an apparently simple question: why are conveyors so important?

As the video shows, the value of a conveyor depends on how it is integrated into the line, the required speed, the operating conditions and the specific production requirements.

The required characteristics also vary significantly depending on the industry: a line dedicated to food or pharmaceutical packaging has different priorities compared to an application in logistics, mechanical engineering or the automotive industry.

This is just one of the topics covered by ConveyorU, a journey dedicated to the different aspects of product handling and packaging line efficiency.

Do you want to improve the efficiency of your line?

Every line has different conditions, products and critical issues. To identify areas for improvement, it is therefore necessary to analyse the process as a whole, looking at how the machines interact and how the product is handled.

The M.H. Material Handling team can help you assess your line, identify any critical points and develop a solution based on the actual needs of your plant.

Contact us to discuss your application and discover how to make your product handling more efficient, continuous and easier to manage.

It happens for different reasons. Sometimes it is a decision made by the purchasing department aimed at reducing costs. Sometimes the end customer requests less plastic. Sometimes it is compliance with new European packaging regulations, such as the PPWR Regulation. Sometimes it is all of these things combined.

Whatever the reason, when the primary film gets thinner, the package becomes lighter and more deformable.

On the conveyor, however, this means less stability.

On the conveyor, just a few microns change everything

A 28-micron film creates a very different pack from a 40-micron one. Lighter and more flexible, it is more affected by any type of contact – whether with product guides or with other packs in accumulation zones. The risk of deformation or overlapping inevitably increases.

Downstream, this results in micro-stops and scrap, and often in complaints from customers receiving damaged products.

The packaging machine continues to run as usual, but the entire section between production and packaging is no longer suitable for the new format. As a result, speeds, chain type, side guides, and contact surfaces all need to be reconsidered, because the entire conveying section must be recalibrated according to the new mechanical properties of the pack.

The buffer that worked yesterday may no longer be suitable today

An accumulation system is designed based on the real parameters of the format, such as weight, rigidity and pack dimensions. When these parameters change – for example, when switching to lighter or more flexible packaging – the behaviour of the product inside the buffer changes accordingly. In a pressure-based system, a less rigid pack therefore risks deformation or damage during accumulation if everything is not correctly set.

The MH Material Handling BAT Buffer operates without pressure on the product and is designed to be flexible and configurable across multiple formats and layouts. This makes it suitable even for lightweight and delicate packs.

However, flexibility does not mean that a single setup works for everything: if the format changes significantly and the buffer is not readjusted, the risk of jams and damage remains.

A useful rule of thumb during the design phase is that a buffer should hold between 2 and 5 minutes of production: the time needed to absorb the typical micro-stops of the line without losing productivity. With lighter formats, however, it is worth recalculating both the effective accumulation capacity and the discharge speed, considering that the downstream machine should be able to run at least 10–20% faster than average to recover the accumulated product.

Downstream of the packaging machine is where the real game is played

When package weight and rigidity change, the requirements of the downstream section of the primary packaging also change. All downstream mechanics – aligners, phases and lane combiners – are suddenly handling a product that is no longer matches the original design assumptions.

The packaging machine keeps running, but the downstream area – the one nobody actively monitors – is where efficiency is lost.

That is why every format change requires a check of the feeding and conveying systems, and it must be done before problems arise.

How to adapt the line without stopping production

The process starts with mapping the characteristics of the new package: weight, dimensions, rigidity and coefficient of friction.

The new format is then tested across every section of the line, not only on the packaging machine, because each section reacts differently and must be checked individually.

The most important step is to involve the conveyor supplier already during the design phase, not once the problem has already become evident.

Working in stages – validating one section at a time before moving on to the next – allows production to remain active while reducing risks.

The format changes. The line cannot stay the same

When a company decides to reduce packaging weight or thickness – whether to cut costs or to meet sustainability requirements – the decision usually starts in the purchasing department. A thinner film is selected, the price is negotiated, and the specification is updated in the system. And then it stops here.

The problem is that no one checks the impact of that change on the packaging line. The process engineer is not involved, at least not immediately. They are called in weeks later, when machine downtime starts to increase, scrap rises, and OEE drops without an obvious cause.

The machine is the same. The product is the same. However, the packaging has changed, and that change affects the entire line: from packaging to accumulation, from conveying to palletizing.

For over 40 years, MH Material Handling has been designing conveying and accumulation systems. We work on layout analysis, buffer configuration, feeding system adaptation, and the integration of new solutions into existing lines, ensuring everything works with today’s format, not yesterday’s.

If you are considering a format change, or if you are already facing issues after a reduction in material thickness, let’s talk before inefficiencies become the norm. A preventive technical discussion costs far less than a stopped line.

It’s 6:45 a.m. The line is down for end-of-shift cleaning. The operator directs a high-pressure water jet onto the conveyor, moving the lance from left to right, then shuts off the valve.

On the surface: clean.

In reality: the frame beneath the belt has three enclosed corners where water never reaches. Organic residue builds up there, day after day.

This is not a cleaning issue. It’s a machine design issue. And the difference between a line that passes a hygiene audit and one that barely gets through – every single time – comes down to this.

Washdown: effective on paper, limited in practice

Washdown – high-pressure cleaning with water and detergents – is the most common response to contamination risks in food processing lines.

It’s relatively inexpensive to implement and provides an immediate sense of control.

The problem is that it only works if the machine has been designed to be cleaned. If the frame has enclosed cavities, if chain returns are inaccessible, if joints retain moisture, the water jet doesn’t solve the issue. It just relocates it. The result is increasing consumption of water and chemicals, longer downtime, and a real risk of cross-contamination. Meanwhile, the quality manager signs off on sanitation reports that, in practice, cannot be fully guaranteed.

Hygienic Design eliminates the problem at the source

Hygienic Design, when applied to machinery, is a design approach that starts with a specific question: how can this machine be thoroughly cleaned, under real operating conditions, with the available personnel, in the shortest possible time?

A conveyor built with this logic features open-frame construction, sloped surfaces for effective drainage, tool-less disassembly, food-grade certified chains, and materials resistant to aggressive cleaning agents.

It’s not “washable” because someone claims it is – it’s washable because there are no areas where residue can accumulate.

From an operational standpoint, the impact is significant: sanitation downtime is reduced, water and chemical usage decreases, and contamination risk is minimized. Hygiene audits become a natural outcome of the design – not a recurring uncertainty.

Not every line carries the same risks – that’s why choosing the right approach matters

In practice, the choice between a Hygienic Design approach and a Washdown system depends on where the conveyor is positioned within the line and the type of product it handles.

For unpackaged products – fresh food, meat, dairy, bakery – the contamination risk is extremely high. Here, Hygienic Design is the minimum requirement.

Monolithic belts with no internal fabric, such as the SaniBelt line we design at MH, are specifically developed for this purpose. They have no exposed textile surfaces that can retain residue and can be cleaned in just a few minutes.

When handling packaged products, still within a white area, requirements change. A washdown design can be sufficient, provided stainless steel construction is maintained and flat surfaces and enclosed cavities are avoided. In this case, tool-less belt removal for cleaning is no longer essential. Moving into grey areas, hygiene requirements can be relaxed further, with greater emphasis on robustness and throughput. Depending on the environment, you may still opt for stainless steel frames – for example, where floors are regularly washed with water – or choose anodized aluminum structures where this is not required.

3 practical steps to quickly identify critical points in your line

Before deciding whether to upgrade a single conveyor or redesign an entire section, you need a simple method to identify where the real issues lie.

Here are three key aspects to assess your current situation:

The first step is to map the line by hygiene risk level

Open product, packaged product, and transition zones. For each area, define the conveyor type and the current cleaning regime.

The second step is to inspect critical design points

Enclosed frame corners, cavities beneath chain returns, joints between modules, and moisture-prone areas. If you can’t reach a spot with a cloth, water won’t clean it effectively either.

The third step is to measure actual sanitation time

If it exceeds 20 minutes per conveyor in high-risk areas, you have a design problem. And remember: no stricter cleaning procedure can compensate for a design flaw.

A layout is designed once -but it’s lived with every day

The issue is that most companies address hygiene only when the problem is already visible: a difficult audit, a product recall, or uncontrolled sanitation costs. At that point, the room for action is limited.

At MH Material Handling, we have been designing conveying systems based on these principles for over forty years. From the Saniflex belt for high-risk areas to the BAT system with USC chain for high-speed lines, every solution starts from a real analysis of the customer’s operating conditions – not from a standard catalog. If your sanitation times are too long, if hygiene audits are always uncertain, or if you are designing a new line, get in touch. We can analyze your processes together and identify the most effective solutions to protect product safety and reduce operating costs.

When designing a packaging line, attention immediately goes to the machines: which packaging machine to choose, what type of labelling machine to install, where to place inspection systems.

However, there is one element that determines the efficiency of the entire system even before thinking about the machines: the layout.

A well-designed layout is almost invisible. Operations flow smoothly, maintenance is quick, and operators move without obstacles.

On the contrary, a poorly designed layout makes itself felt every day, with downtime, bottlenecks, cleaning difficulties, and waste of space and time.

Many issues that seem to originate from the machines actually arise during the layout design phase.

A recurring machine stoppage at the same time every day, for example, may not be due to a technical fault, but to a buffer positioned in the wrong point of the line.

A cleaning process that takes twice as long as expected may be the result of conveyors placed too close to each other, not a surface sanitization issue.

Operators losing valuable minutes moving materials from one area of the line to another may indicate a flow design error, not a lack of staff.

The layout determines how machines interact, how materials move, and how operators work. And when the layout is wrong, even the best machines struggle to perform at their full potential.

Let’s look at the most common mistakes that compromise the performance of a food processing line.

1.   Underestimating space for maintenance and sanitation

This is one of the most frequent mistakes: machines and conveyors positioned too close to each other, without considering that they will need to be accessed for cleaning, inspection, and component replacement.

In the food industry, this becomes a critical issue, as sanitation is not an occasional activity but an integral part of daily operations.

If a conveyor belt is trapped between two machines with insufficient lateral space, cleaning becomes superficial. Operators struggle to reach critical areas, downtime increases, and hygiene risks grow.

Even the most advanced Hygienic Design loses effectiveness if the layout does not support it. An open frame designed for drainage is of little use if there is no physical space to access the surfaces to be cleaned. For this reason, it is essential to consider not only the machine itself, but also the operational space around it: the room needed to open frames, remove components, allow operators to access with cleaning equipment, and move freely during sanitation procedures.

2.   Ignoring material and operator flows

An efficient layout defines clear paths. Raw materials, semi-finished products, finished goods, and waste must each follow a precise flow, ideally unidirectional, from “dirty” to “clean”. When these flows intersect, the risk of cross-contamination increases exponentially.

The same applies to operator movement. If reaching a quality control station requires crossing the entire line and passing near the waste discharge area, there is a design flaw.

Every unnecessary movement is lost time and a potential food safety risk.

Physical separation between areas with different hygiene levels should be planned from the outset. The positioning of buffers and accumulation systems also makes a difference: a BAT Buffer placed in the right position can absorb downstream micro-stoppages without blocking the entire line. Placed incorrectly, it becomes just an obstacle.

3.   Failing to plan for flexibility in format changes and future expansion

Food processing lines are not static. Formats change, production evolves, and volumes grow. Yet many layouts are designed without considering future developments. As a result, when it’s time to introduce a new format or add an inspection station, physical constraints become a barrier. There may be no space to integrate new elements, even if the modularity of conveyors would allow it.

Modularity is not just a feature of machines—it is a design principle that should also guide layout planning.

Systems like BAT are built on this logic: standard components that adapt to different configurations.

However, the layout must also include “growth areas” identified from the beginning—spaces where buffers, additional stations, or line diversions can be added.

Planning for flexibility may involve a slightly higher initial cost, but it leads to significant savings in the medium term, when production changes can be implemented in hours instead of weeks of downtime.

4.   Choosing the wrong accumulation system (or not including one at all)

Every line includes machines operating at different speeds. Without an accumulation system, even a micro-stoppage of a few seconds can halt the entire production flow.

Yet many layouts either do not include buffers or size them incorrectly.

An oversized buffer takes up valuable space without delivering real benefits.
An undersized buffer cannot absorb flow variations and becomes ineffective.

Then there is the choice of system type: accumulation systems with product-to-product contact can damage fragile items such as biscuits or packaged snacks, even when using low-pressure solutions.

The BAT Buffer was developed precisely to address these issues: compact, zero-pressure accumulation that ensures operational continuity even during micro-stoppages.

However, the key point is this: buffers must be planned during the layout design phase and positioned strategically—not added later as a patch once problems arise.

5.   Overlooking heights and elevation changes

It may seem like a minor detail, but operating heights make the difference between an efficient line and one that strains operators. Conveyors placed too high or too low force unnatural postures, increase the risk of errors and injuries, and slow down operations.

Height differences between conveyors must also be carefully calculated.

A sudden drop can destabilize fragile or unstable products.

In some cases, when horizontal space is limited, spiral conveyors provide an effective solution, allowing elevation changes without occupying valuable floor space.

Ergonomics becomes an investment that translates into fewer errors, fewer stoppages, and higher productivity.

And it must be considered from the layout design phase—not added later with stairs, platforms, and walkways that complicate the system and increase costs.

The layout is designed once, but its impact is experienced every day

An effective layout is not the result of compromises between existing constraints—it is a strategic choice that impacts the efficiency, safety, and scalability of a packaging line for years.

Design mistakes come at a cost every single day: downtime, waste, operational difficulties, and complex maintenance. And in many cases, these are avoidable errors—preventable with a broader perspective and collaboration with experts who understand the production dynamics of the food industry. At M.H. Material Handling we support our clients from the earliest layout design stages, combining conveyor system supply with consultancy that starts from flow analysis and extends to space optimization. If you are designing a new line or looking to improve an existing one, get in touch with us: we can assess the most effective solutions for your plant together.

Insights, ideas and news
about product handling