M.H. – Material Handling

Luca Fontana

Today’s food packaging lines are increasingly fast, automated, and high-performing. Individual machines can reach speeds and accuracy levels that were unthinkable just a few years ago.

And yet, in many plants, higher performance does not translate into a real improvement in overall line efficiency.

The reason is simple: a packaging line is not the sum of its machines, but a dynamic system where each station directly affects the others.

It is precisely within this delicate balance that the most common issues arise: unplanned downtime, micro-stoppages, and cascading slowdowns.

In this context, accumulation systems are no longer just an accessory—they are a key element that can truly make the difference in packaging line performance.

The accumulation system: the “lung” of the line

A useful way to understand the role of accumulation is to think of it as the “lung” of the packaging line—this is exactly how we at M.H. Material Handling define it.

An accumulation system is designed to “give breathing space” to the line, absorbing speed variations and temporary stoppages while maintaining a continuous product flow.

When a downstream machine slows down or stops (for example, during a reel change or adjustment), the accumulation system buffers the excess product, preventing upstream machines from stopping.

When the line restarts, the accumulated product is released in a controlled way, allowing partial recovery of production without stressing the system.

A simple principle, yet with a significant impact on overall line productivity.

The problems accumulation systems solve

In many packaging lines, certain inefficiencies are often accepted as unavoidable. In reality, they are frequently the result of missing or improperly sized accumulation.

1. Reel changes and line stoppages

Every film or packaging material change requires a machine stop. Without an accumulation system, this stop propagates across the entire line, halting even the sections that could otherwise keep running.

2. Different machine speeds

It is rare for all stations in a line to operate at the same speed.

Performance differences generate continuous micro-stoppages that negatively impact the entire process. Even small variations create instability, increasing component wear and reducing process predictability.

This is exactly where accumulation systems come into play.

Why accumulation is even more strategic today

While accumulation used to be considered optional, it has now become a strategic design choice. This is due to several factors:

  • higher line speeds
  • greater product variability (formats and packaging types)
  • limited available space (especially in existing plants and especially in Italy)
  • increasing pressure on overall system efficiency.

In this scenario, accumulation becomes a balancing tool, enabling smoother and more predictable product flow.

How to choose the right accumulation solution

One of the most common mistakes is to consider accumulation as a module to be added at the end of the line. In reality, its effectiveness depends on how it is designed and integrated into the system

Key factors to consider include:

  • product type and its resistance to pressure
  • line speed and differences between machines
  • available footprint and vertical space
  • required operating logic (FIFO or LIFO)
  • working environment (e.g. maintenance and cleaning requirements)

Only by starting from these elements is it possible to define the most suitable accumulation solution, avoiding compromises that become costly over time.

Ultimately, designing accumulation means designing production continuity and line reliability. It cannot be treated as a standalone element: it must be developed based on line configuration, product flow, production targets, space constraints, and real operating conditions.

With M.H. Material Handling, this evaluation is carried out through a structured approach. Thanks to the M.H. Solution Scan, we analyze your packaging line in detail to identify critical areas and determine if, where, and how an accumulation system can improve operational continuity, reduce downtime impact, and increase real process efficiency.

Contact us to request the M.H. Solution Scan and discover how to make your packaging line more stable, efficient, and ready to handle daily production variability.
When it comes to “Hygienic Design”, many people immediately think of stainless-steel equipment, free of gaps and easy to wash down.
This is a correct image — but only a partial one.

The reality is that Hygienic Design does not start — and does not end — with the equipment.
It is a structured approach that takes shape much earlier, beginning with how the facility is conceived, built, and organized.

Only by considering the entire production ecosystem — from building structures and material flows to raw material handling and personnel procedures — can safety, efficiency, and sustainability be truly ensured.
Machines come later: their role is to protect and preserve what has been designed upstream, not to compensate for shortcomings at earlier stages.

The facility as the first link in the chain

Every Hygienic Design project therefore starts with the building layout.

Its location in relation to the external environment, the distance from potential sources of contamination, floor slopes designed to promote proper drainage, and thermal insulation all directly affect the ability to maintain hygienic conditions.

Selections of materials is equally critical: walls and surfaces must be easy to clean and durable over time

If a facility is not designed with these principles in mind from the outset, the cost will be significant: more washdowns, higher water and chemical consumption, and increased operating costs.

This is not a problem that can be solved with a high-quality machine alone, but with couscous design decisions made from the very beginning.

People, raw materials, and products: the flows that make the difference

The second level focuses on internal movements.

Ingredients, semi-finished products, and personnel must not share high-risk pathways. Any overlap increases the likelihood of cross-contamination.

For this reason, more advanced manufacturers implement a hygienic segregation of production areas, physically separating high-risk zones from low-risk ones and enforcing strict procedures: garment changes, controlled access points, and physical barriers. This approach, commonly referred to as hygienic zoning, is one of the most effective tools for reducing contamination risks within food processing facilities.

Machines are the protagonists, but procedures are the script

Only at this stage does the focus shift to machinery. Their role is not to “create hygiene,” but to preserve the hygienic conditions established upstream.

Features such as cleanable surfaces, open-frame designs, tool-free removable components, and food-grade certified materials are not optional details — they are essential requirements. A single poorly designed critical point is enough to turn a machine into a source of risk.

The cost of a mistake can be substantial: Commercial Food Sanitation estimates that a product recall caused by contamination costs, on average, €1.67 million in operational losses and reputational damage.

This is why Hygienic Design is not a technical detail, but a strategic investment.

We don’t sell machines — we design safety

At MH Material Handling, we believe that Hygienic Design is not something to be applied downstream, but a philosophy that must guide every decision throughout the entire process. This is why, although we specialize in the design of conveyor systems such as Saniflex, we do not limit ourselves to supplying a machine.

Our consulting approach always starts with a comprehensive analysis of the plant: we assess layout, material and personnel flows, sanitation practices, and production requirements in order to integrate the conveying solution into a context that is truly coherent, safe, and efficient.

Saniflex is not an off-the-shelf product, but a modular and customizable system, engineered to simplify cleaning, withstand aggressive detergents, and ensure operational continuity.

What truly makes it effective, however, is its ability to fit into a broader approach in which every design choice contributes to reducing risks, costs, and operational complexity.

Would you like to understand whether your line truly complies with Hygienic Design principles — and how Saniflex can enhance it to the fullest?

Contact us for a tailored consultation: together we will analyze your processes and identify the most effective solutions to protect product safety and strengthen your business competitiveness.

It already works well as it is… do we really need to change?

This is the question many plant managers ask themselves when they look at their packaging line.

If the machines are running, orders are being fulfilled, and production continues, why intervene in something that appears to be working?

The truth is that “working” does not always mean “working at its best.”

A small bottleneck, an unexpected buildup, one manual step too many: details that often go unnoticed, yet over time erode productivity, margins, and delivery reliability.

Today, the efficiency of a line is not determined by the power of individual machines, but by the ability to integrate and harmonize every component into a balanced, seamless flow.

Conveyors: the circulatory system of the line

Just as blood carries oxygen through the body, conveyors represent the circulatory system of a packaging line.

They are responsible for synchronizing machinery, absorbing fluctuations, and preventing bottlenecks.

If the flow is not continuous and well balanced, even the most advanced machine loses its effectiveness and the risk of downtime increases.

Yet these systems are often underestimated already at the design stage, resulting in inefficiencies that are difficult to correct later on.

Different solutions for different needs

At M.H. Material Handling, we know that no two lines are the same. That is why our solutions are designed to adapt to very different products, spaces, and processes.

Heliflex LIFO Spiral System

Ideal for large product accumulation with heights not exceeding 90 mm. This double-spiral system finds its optimal sizing with between 200 and 500 meters of available space.

BAT-Buffer Modular System

Modular and compact, it is perfect for handling different product types and plant layouts. It is versatile, easy to integrate into existing lines, and has relatively limited footprint requirements. Its ideal size ranges between 100 and 150 meters of available space.

5L FIFO Multilayer Belt

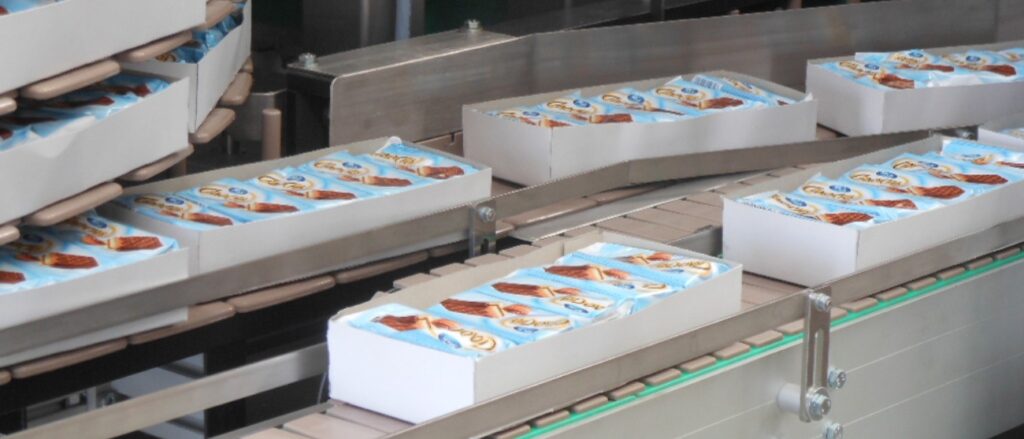
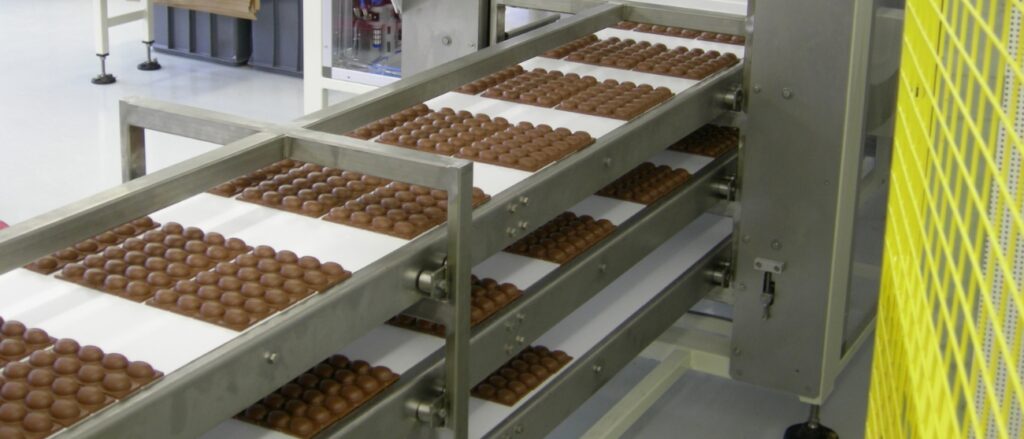
Developed specifically for the confectionery sector, it enables gentle multilane transport upstream of the packaging stations, reducing the risk of product damage.

These solutions are complemented by mergers, dividers, elevators, and intelligent handling units, all designed to ensure increasingly smooth and fully integrated material flows.

Efficiency is much more than speed

Being efficient today does not simply mean “running faster.”

It means designing ergonomic lines that are easy to clean, hygienic, and capable of making the most of the available space.

It means having systems that reduce downtime, optimize energy consumption, and ensure a long-term return on investment.

Our solutions, entirely made in Italy, reflect these values: they are reliable, customized, and built to last.

With nearly forty years of experience in the food and pharma sectors, at M.H. Material Handling we do more than supply individual components.

We always start with layout consulting, analyze material flows, and develop integrated conveying and buffering solutions that transform plants into efficient and competitive ecosystems.

Our goal is simple: to help companies increase productivity and stability while reducing complexity and hidden costs.

If your line “already works well,” ask yourself: is it really expressing its full potential?

A custom-designed conveying system can make the difference between a line that merely runs and one that grows.

Contact us for a personalized consultation and discover how to make your plant more fluid, safe, and efficient—without disruptive changes.

Today’s production lines demand increasingly high standards: higher speeds, lower noise levels, and greater safety.

The historic 879 chain, developed in the late 1980s and established as an industry benchmark, has long proven its strength as a tireless “workhorse” of conveyor lines.

MH Material Handling decided not to settle.

Drawing on nearly forty years of experience and direct, ongoing dialogue with field technicians, USC – UltimateSafeChain was created: an evolution that preserves the robustness of the 879 while integrating with new technologies to meet the real demands of modern industry.

Can something that already works perfectly really be improved?

The strength of the 879 BAT has never been in question: robust, versatile, andlong-lasting, it has earned the trust of operators because it “simply works.”

In particular, tangential drive has proven over time to be the most effective solution for managing LIFO accumulation systems, such as the BAT Buffer, ensuring stability and operational continuity.

However, through extensive field experience and ongoing dialogue with technicians, a key insight emerged: when the foundation is solid, it can be made even safer, quieter, and more efficient.

For this reason, we partnered with Ammeraal Beltech, integrating Safety Finger technology into our new USC chain, a solution already recognized for its strong focus on operator safety.

USC: the reliability you’ve always trusted, even better performance

The new UltimateSafeChain is not a break with the past, but its natural evolution.

It is fully backwards-compatible with existing lines: no system redesign is required—only the chain and sprockets need to be replaced.

The tangible benefits are immediate:

  • Higher operating speeds, increasing productivity without compromising stability.
  • Reduced noise levels, improving operator comfort and supporting compliance with industrial noise regulations.
  • Greater installable length, enabling more flexible and scalable system layouts.
  • Enhanced stability and safety, thanks to the integration of Safety Finger technology, which reduces the risk of accidents and unexpected stoppages.

All of this while preserving what operators already know and value: the reliability of tangential drive, a distinctive feature that continues to deliver top performance in buffering and accumulation systems.

Easy revamping that reduces downtime and hidden costs

One of the most critical aspects of plant modernization is the risk of downtime. Stopping a production line to replace components slows productivity and increases operating costs.

USC was developed with a clear objective: to simplify revamping.

No complex rebuilds, no full replacement projects—just the new chain and the corresponding sprockets are enough to transform an existing system into a more modern, efficient, and safer solution.

This approach fully aligns with the Total Cost of Ownership (TCO) perspective: investing in next-generation components helps reduce hidden costs related to extraordinary maintenance, energy consumption, and unplanned downtime.

Why choose MH Material Handling

At MH Material Handling, every innovation is driven by listening to the real needs of industrial systems.

With USC, we chose to preserve what already works—the robustness and tangential drive of the 879 BAT—and enhance it with new technologies that address today’s requirements: higher speed, greater safety, lower noise, and improved efficiency.

This is not an “off-the-shelf” product, but a solution designed to last over time, reduce risk, and simplify the daily work of those who operate and maintain systems.

That is what sets us apart: transforming conveyors from simple components into true drivers of competitiveness for companies.

If the 879 BAT has been a cornerstone for nearly 40 years, USC – UltimateSafeChain marks the beginning of a new chapter: the same reliability, with higher performance.

Would you like to find out whether USC can make your line more efficient and safer without redesigning the system?

Contact us for a personalized consultation: together, we will assess how a simple upgrade can be turned into an immediate advantage.

At first glance, it may seem like a small detail, just a component connecting one machine to another, nothing more.

In reality, the conveyor is the heart of the line: efficiency, hygiene, safety, and ultimately the quality of the product reaching the consumer all depend on it.

Yet too often, its selection is underestimated, as if one belt were as good as another. But that’s not the case.

Each application is different, every product has its own characteristics, and each plant has its own criticalities.

Treating the conveyor as a “standard” element means opening the door to unexpected downtimes, contamination, waste, safety issues, and hidden costs that grow over time.

A significant share of line stops doesn’t stem from mechanical failures but from synchronization and accumulation problems, a clear sign that conveyors impact production continuity much more than people think.

When the product is “naked” fresh or dry is not enough

Talking about “naked” products means addressing very different worlds. A dry croissant is not the same as a honey-covered bar, just as a filled cake slice cannot be compared to a cracker.

In the fresh sector, hygiene is paramount. Belts must be washable, cavity-free and easy to sanitize. Belts with internal fabric layers are not suitable: if the fabric emerges, it becomes impossible to clean properly.

That’s why monolithic belts are used, more rigid and less flexible, but capable of ensuring the highest hygienic standards.

In the dry sector, the range is broader: brittle products such as biscuits or crackers fit well on modular chain conveyors, which allow easy removal of crumbs.

But when coatings, creams, or jams come into play, PU belts are required, surfaces that can be scraped clean without damaging the belt.

Each product type therefore requires a targeted evaluation.

Packaged products, but where in the line?

Even a packaged product raises specific questions: is it located in a white zone or a grey zone? Does it require washdown capability or not?

Are high speeds, tight transfers, or low noise levels needed?

In general:

  • The tabletop chain conveyor is ideal for heavy loads, high speeds, and complex layouts.
  • The modular chain conveyor offers greater flexibility and smaller wrap diameters, but it’s less robust, has wider curve radii, and requires more maintenance attention.

If we’re in a washdown area, the structure matters too: at least the legs must be in stainless steel, if not the entire frame.

The choice, therefore, concerns not only the belt, but the whole operational context.

The invisible factors that make the difference

Beyond product features and packaging type, there are less visible but decisive variables:

Belt position

On the floor or overhead?

Overhead systems prioritize robustness, since maintenance interventions are more complex.

On-floor conveyors, instead, prioritize operator safety, requiring reduced-pitch chains to minimize risk.

Maintenance

How often will the belt need to be serviced? High frequency calls for easily removable and sanitizable designs.

Format variety

If the line handles multiple product types, flexible and adaptable systems are essential.

Finally, one basic principle must not be forgotten: machines never work in perfect synchronization. That’s why accumulation systems (buffers) are necessary to guarantee continuity and prevent line stops.

At M.H. Material Handling, we know these complexities well. For nearly forty years, we have been designing tailor-made conveyors for every type of line, product, and requirement – from fresh to packaged good.

Our solutions always start from listening: we don’t begin with a standard catalog, but with a real customer problem.

Whether it’s about handling a delicate product, freeing up floor space for operators, or optimizing flows in limited spaces, every project is co-designed together with the customer.

From the washdown SaniFlex line to the BAT system with USC chain, up to the ModulFlex conveyors with modular chains ,each technological choice follows a clear logic: transforming daily challenges into efficient, safe, and long-lasting solutions.

For us, automation doesn’t mean selling a machine, it means designing together the right answer to a real need.

Want to understand which solution best fits your line?

Contact us for a personalized consultation and discover how to make your system smoother, safer, and more efficient.

Increasing the performance and efficiency of your production line often requires a significant investment in both money and space.

However, there are aspects of your packaging line that can be optimized to make the most of the available space and boost productivity — all while staying within your planned budget.

Streamlining the product flow through your packaging process allows you to enhance the productivity of your entire production line. With the right solution, you can achieve this while respecting space constraints and maintaining sustainable costs.

If you want to find out which solutions best suit your needs, contact us and request our MH Scan Solution service: we will analyze your packaging line to identify how to refine and optimize your production setup.

In the food industry, hygiene isn’t just good practice—it’s an essential requirement for ensuring safety, quality, and regulatory compliance.

But is designing machines that are “easy to clean” really enough?

The answer is no.

Preventing contamination and protecting the end consumer requires a much more advanced, structured, and systematic approach.

That’s why today we’re talking about Hygienic Design: a set of construction criteria, design choices, and specific materials developed to eliminate risk areas, simplify sanitation, and guarantee the highest standards in food safety.

Hygienic Design in the Spotlight: Why It’s Transforming Food Production

In recent years, tighter regulations and a growing focus on food safety have brought Hygienic Design to center stage.

Food manufacturers are dealing with increasingly automated processes—and maintaining high hygiene standards throughout the entire line, including the most complex phases like internal transport and handling, is now a top priority.

Key challenges include:

  • Preventing cross-contamination, both microbiological and chemical.
  • Ensuring fast and effective cleaning of every product-contact surface.
  • Reducing water and detergent consumption to meet both sustainability goals and cost control.
  • Complying with EHEDG (European Hygienic Engineering and Design Group) guidelines, now a benchmark across the European industry.

Hygienic Design Is More Than Just Stainless Steel

Many think Hygienic Design simply means using stainless steel—but that’s only part of the story.

A proper approach starts with material selection but extends to surface geometry, accessibility for cleaning, the absence of gaps and stagnation areas, and tool-free disassembly of washable components.

Among the most common materials, AISI 304 stainless steel with bead-blasted or 2B finishes is standard for frames and load-bearing structures.

But plastic materials also play a key role. For instance, M.H.’s Saniflex system uses polypropylene chains with polyketone pins—highly resistant to the chemical agents used during sanitation.

Saniflex: Designing Hygiene with No Compromise

M.H. Material Handling developed the Saniflex system specifically to meet the toughest requirements of the food industry, particularly in dairy production.

In these environments—where processing fresh and packaged cheese demands absolute cleanliness—standard solutions simply aren’t enough.

Saniflex stands out thanks to:

  • Fully open frame design that prevents build-up and supports efficient drainage.
  • Tool-free removable components for fast and easy daily or deep cleaning.
  • Chains resistant to aggressive detergents but fully compliant with food-grade regulations.
  • Reduction in water and detergent use compared to traditional systems.

The result?

A solution that enhances productivity, guarantees hygienic safety, and supports environmental sustainability targets.

Invisible Contamination: The “Forever Chemicals” Risk

Hygienic Design isn’t just about bacteria and mold.

Today, manufacturers must also consider chemical contamination from persistent substances like PFAS (per- and polyfluoroalkyl substances), often called “forever chemicals.” These may come from the environment, industrial coatings, or even the detergents used on production lines.

Designing equipment that’s easy to clean also means reducing surface exposure to these chemicals.

With Saniflex, manufacturers can:

  • Reduce washing cycles.
  • Use gentler, less aggressive detergents.
  • Minimize the risk of transferring harmful substances onto the product.

When Hygienic Design Becomes a Competitive Advantage

Hygienic Design is a strategic investment that brings measurable benefits:

  • shorter downtimes,
  • longer equipment lifespan,
  • lower cleaning costs,
  • stronger food safety,
  • regulatory compliance.

At M.H. Material Handling, these principles are a cornerstone of our engineering.

With solutions like Saniflex, we combine technological innovation, operational efficiency, and full adherence to the strictest international guidelines.

Wondering if your production line meets today’s hygiene standards?

Book a free consultation with our experts via our MH Scan Solution service: we’ll assess your system’s critical points and show you how to optimize safety, efficiency, and sustainability.

Switching to sustainable packaging is never easy: it requires time, investment, and careful planning.

One aspect that is often underestimated is the adaptation of conveying systems: without modern solutions, you risk ending up with innovative packaging but a slower and less efficient production process.

At MH, we are constantly committed to supporting you in making your packaging more sustainable. In particular, for the conveying part we offer solutions such as the Magic Sorter or the Intralox END system, both ideal for handling the new types of sustainable packaging.

In addition, with our MH Scan Solution – an in-depth analysis service of your packaging line – we help you optimize the production layout with a view to sustainable packaging.

Contact us to discover how to get your line ready for change.

In the packaging industry, where every interruption can result in productivity loss, accumulation systems become strategic components to maintain performance and output. One ideal solution is the BAT Buffer by M.H. Material Handling, which we explore below.

The Heart That Keeps Your Line Alive

The BAT Buffer operates using a LIFO (Last In, First Out) logic and is designed to manage micro-stoppages typical in packaging lines. In the event of a downstream stop, the system automatically diverts incoming products to the accumulation buffer, keeping upstream machines running.

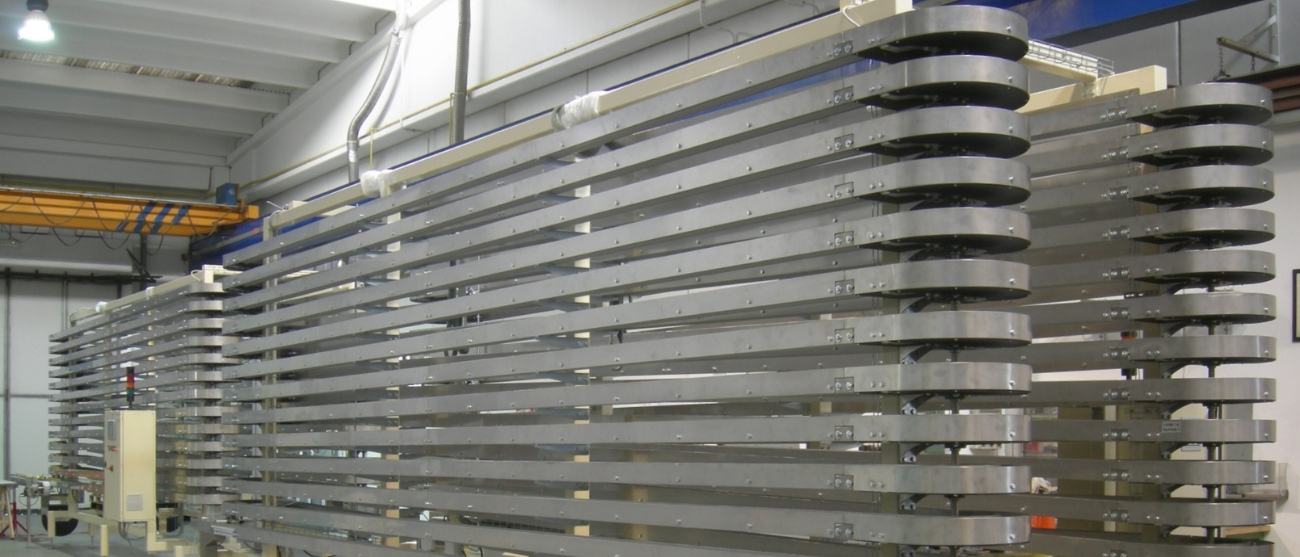
The BAT Buffer features a spiral structure that alternates straight and curved sections. This design maximizes available space, offering up to 150 meters of accumulation capacity with a single motor. The straight sections range from 2.5 to 6 meters, while the curves have an average radius of 200 mm, allowing adaptation to complex layouts.

Precision Control, Down to the Millimeter

During loading, products are guided into the buffer with a consistent pitch, regulated via inverter, preventing overlaps or damage—crucial for delicate or pressure-sensitive packaged goods.

Once normal operations resume, the BAT Buffer reverses direction and gradually releases the products back into the production flow. This can be done via an orthogonal transfer unit (to maintain product orientation) or a dynamic combiner for high-speed lines.

The average emptying time, from a full configuration, ranges from 15 to 25 minutes depending on installed capacity and downstream speed.

Recover What You Thought Was Lost

One of the BAT Buffer’s standout features is its ability to recover production lost to micro-stoppages. If downstream machines have an extra 10-20% capacity, the system can completely eliminate these losses by the end of a shift.

Its mechanical structure also enables quick switching between loading and unloading phases without needing full accumulation, helping to regularize the production flow. This operational flexibility makes it ideal for lines subject to frequent format changes or sudden production peaks.

Engineered to Fit, Wherever Needed

The BAT Buffer is ideal in sectors where output sequencing is not critical:

  • Bakery and confectionery products
  • Coffee and vacuum-packed goods
  • Other long shelf-life items

The structure is available in anodized aluminum for standard applications or AISI 304 stainless steel for environments requiring higher hygiene standards, such as cleanrooms. It supports occasional washing without compromising performance.

Its pressure-free design and modular components make it suitable for integration into existing plants, facilitating revamping operations.

See It Live

For those interested in discovering the BAT Buffer’s full potential, M.H. Material Handling will be exhibiting at IPACK-IMA 2025 in Milan from May 27 to 30, Pavilion 7, Booth B21.

For the first time in Italy, the compact infeed/outfeed system of the BAT Buffer—already praised at FachPack 2024—will be presented. Visitors will also get a sneak peek at an exclusive feature designed for those who recognize technical evolution at first glance.

In the packaging industry, sustainability is no longer an option, but achieving it inevitably involves additional costs.

Automation can provide a concrete solution: by improving the efficiency of production lines, it helps offset the costs required for sustainability, becoming a strategically.

This, of course, requires taking into account three key variables that determine the success of a project.

Integrating automation systems is not always straightforward: structural constraints and limited space often come into play, requiring creative and innovative solutions.

True success comes from finding the right balance between investment, productivity, and space optimization.

This is why at MH we support our clients with MH Scan Solution: our design approach that starts from the very beginning, considers all variables at play, and guides automation toward the best possible outcome.

Insights, ideas and news
about product handling

A divider distributes a product flow across multiple outlets along a packaging line. One of the most common situations arises when an upstream machine has a higher capacity than the downstream machines and the flow needs to be split into multiple lanes. This is typical of high-speed and flowpack lines, at the transition from primary to secondary packaging. We have been working in this field for over forty years, across the food, beverage, pharmaceutical and packaging sectors.

On these lines, the main parameters are line speed and cadence. Beyond a certain output rate, even the fastest secondary packaging machines cannot keep up. This is the same limitation encountered with mergers.

Splitting the flow into multiple lanes also helps ensure machine reliability and durability over time. Downstream, this may mean using several product arranging units or a single pick-and-place machine operating on multiple lanes simultaneously.

Diverter or sorter? Understanding the differences

The term divider, however, covers different types of equipment. The most immediate distinction is between a diverter and a sorter.

A diverter sends identical products into different lanes without changing how the products themselves are handled.

A sorter, by contrast, can also separate products according to specific criteria. Different boxes are directed to different outlets and are not treated identically, because a particular code or product is routed to its designated outlet. From a design standpoint, a sorter consists of a straight conveyor section with lateral outlets.

The 7 parameters that influence the choice

Deciding whether you need a diverter or a sorter is only the starting point. Before comparing technologies, it is worth establishing the following:

  1. the nature of the product: its shape, stability, fragility and deformability,
  2. line speed,
  3. cadence,
  4. the number of outlets required,
  5. whether the product can be touched,
  6. whether it can withstand pressure,
  7. product dimensions.

The most common solutions and when to use them

The deciding factor is the number of outlets. The selection criteria change significantly between a one-to-two divider and a multi-lane system.

Multi-lane systems require at least a channel-system divider, suitable for products that can come into contact with one another. Because contact is permitted, the divider does not space the products at set intervals: instead, it stops them in the channel, allows them to accumulate, and then switches channels. A multi-channel solution can still be considered for fragile products, but only when it is absolutely certain that the preceding product has cleared the channel.

In multi-lane flowpack systems, we use a sequence of one-to-two dividers. The application becomes more complex when products are fragile or low-profile, with a risk of overlapping.

A flap divider moves the product by making contact with it, provided the product can tolerate this. It is limited to two outlets: to obtain more, several finger-type dividers are generally arranged in a cascade. This is the simplest and therefore least expensive solution. Essentially, it consists of a deflecting paddle, with the limitations described above.

The soft touch system guides the product gently and is used on flowpack lines where accumulation is not possible. This solution also normally operates with one inlet and two outlets.

For robust, stable products such as cartons, boxes or trays, a mechanical multi-lane divider is a good solution, directing the flow by means of pallets, mobile channels or drawers.

Special solutions and when they make sense

Magic Sorter

When a product is very flat, thin or deformable, side guides can become a problem. The product may slip between the guide and the conveyor surface and become jammed.

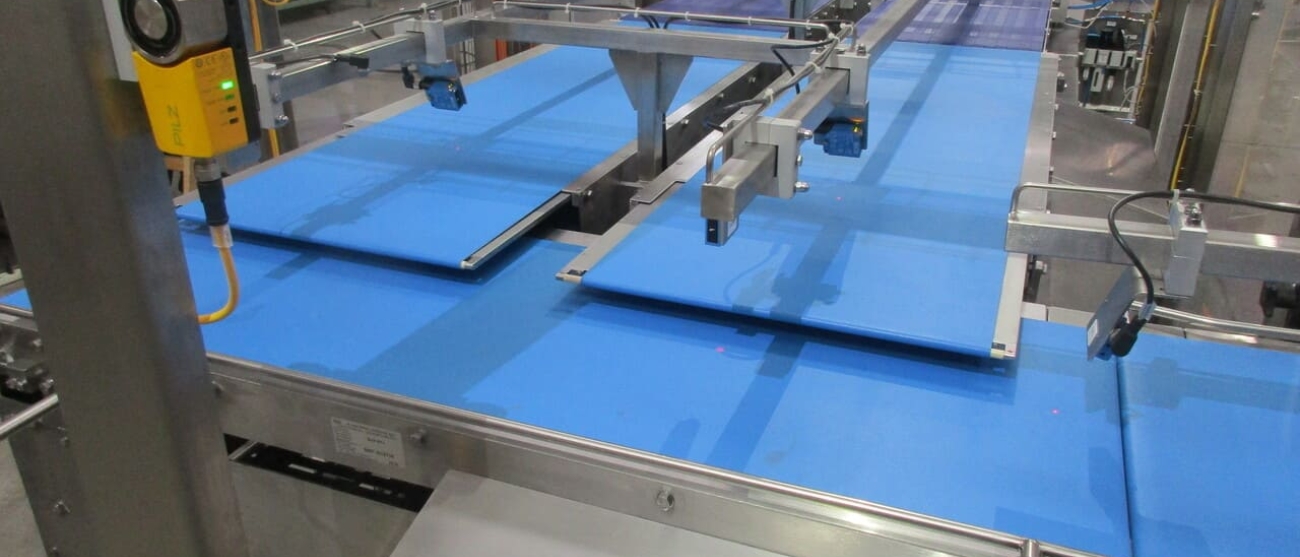
In these cases, M.H. uses the Magic Sorter as either a divider or a merger. Product movement is controlled by a modular chain with embedded balls, suitable for items that cannot be handled using conventional side guides.

The Magic Sorter also makes it possible to create multiple outlets with the same system. This flexibility does, however, come with a throughput limitation: in the fastest applications, it can handle approximately 120 pieces per minute, which is lower than the throughput achievable with other sorting technologies.

AIM

AIM combines a modular conveyor belt with a pneumatically actuated, recessed pusher. The system acts on the lower part of the product, moving it through contact with its side. It is therefore suitable for non-deformable items that can withstand lateral contact.

Its main advantage is washdown suitability. The pneumatic actuation system withstands frequent washing, particularly when a dedicated stainless-steel cylinder is used. AIM can achieve an indicative maximum throughput of 120 pieces per minute.

Like the Magic Sorter, AIM is not used on flowpack lines: the small size of the products prevents the balls or the pusher from controlling them properly. In this case, the limitation is related to product dimensions, not line throughput.

ARB

ARB is a solution intended exclusively for end-of-line applications, where larger products such as boxes and other packages ready for subsequent processing stages are handled. One of its most common applications is feeding palletisers.

Product size alone is not enough to determine whether it can be used. The contact surface must also be checked: the bottom of the product must be even. This technology therefore requires specific conditions and differs from the dividers used between primary and secondary packaging.

Cost is another factor in the decision. ARB requires a higher investment and would not be justified where a simpler solution can perform the same task. It is therefore considered when the product type and end-of-line application genuinely warrant its use.

How to choose the right divider

Once these points have been clarified, the most suitable technology becomes much easier to identify.

Without this analysis, there is a risk of choosing a divider based on throughput alone, overlooking product characteristics, pressure resistance and the operating environment.

At M.H. Material Handling, we design and integrate all these solutions, from mechanical multi-lane dividers and the Magic Sorter to Intralox ARB and AIM applications. We support our customers in analysing product flows and selecting the most suitable configuration.

If divider selection is still an unresolved aspect of your project, we can assess it together, considering the product, throughput and required destinations to identify the best solution.

How many types of conveyors are there, and how do you choose the most suitable one for a specific application?

In this episode of ConveyorU Academy, our mascot Convy asks Luca Fontana, CEO of M.H. Material Handling, who walks us through the main conveyor technologies available and the key factors to consider when making the right choice.

The most suitable conveyor depends on the type of product, the stage of the production process, and the characteristics of the line.

That’s why there is no single best technology for every application: it’s essential to find the right balance between different requirements, such as safety, speed, and the characteristics of the product being handled.

Want to improve your production line’s efficiency? Contact us and request a no-obligation MH Scan Solution consultation. We’ll help you analyze your application, identify potential issues, and develop a solution tailored to the actual needs of your facility.

Chocolate is irresistible. Less so when it ends up sticking to the conveyor belts on your production line.

In the chocolate and confectionery industry, sugar-based residues can make conveyor cleaning particularly challenging, especially when products move through multiple processing stages before reaching the packaging area.

At M.H., in collaboration with Steam Italy, we have developed a cleaning system designed for different conveyor configurations, from continuous-surface monolithic belts to modular plastic chains.

Different conveyor types come with different characteristics and cleaning requirements, which means they also require different cleaning approaches.

Do you have a specific cleaning challenge on your production line? Contact us: we can assess your conveyor configuration together and identify the most suitable solution.

A high-quality packaging line can deliver reliable performance for decades, especially when supported by careful engineering and proper maintenance.

The service life of a system represents significant value, but being fully operational does not always mean it can meet today’s production, technological and regulatory requirements.

New packaging materials, sustainability goals, and increasingly demanding industry standards require systems capable of evolving – a particularly important consideration in the food industry, where hygiene, ease of cleaning, and safety are fundamental requirements.

Do you want to learn how to adapt your system to new regulations and changing production requirments?

Contact us for a technical consultation.

Converging multiple product lanes into a smaller number of lanes may seem like a simple operation. In reality, the way products are collected, timed and delivered to the downstream machine can have a significant impact on the consistency of the entire process.

This is why designing a lane merger is not simply a matter of considering line speed. First of all, it is necessary to understand how the product behaves: its shape, stability, fragility, ability to run in contact with other products, and the pitch required by the downstream machine are all factors that help define the right solution.

Based on these parameters, M.H. Material Handling designs the merging configuration best suited to the characteristics of the line and the product.

The first criterion is the product: can it withstand accumulation?

Even before speed is considered, the assessment starts with the product and its ability to withstand accumulation.

A product that can tolerate accumulation can withstand the pressure generated by products touching and pushing against one another. Boxes, trays and products stacked in tightly packed formats fall into this category.

A fragile product, or one prone to overlapping, cannot withstand this type of stress, and a pressure-based system could compromise its integrity.

This is why resistance to accumulation is the first factor to be assessed, as it determines whether a pneumatic or dynamic lane merger is required even before line throughput is considered.

There is, however, one useful exception to bear in mind.

Even with a product that can withstand accumulation, the presence of many formats with significantly different widths often makes a dynamic solution preferable. This avoids format changeovers using adjustable or automatically controlled guides and, because the products do not come into contact with one another, eliminates the risk of misalignment.

Pneumatic, DU Series or HP Series: the right technology for each product

A pneumatic lane merger is the simplest and most cost-effective solution, but it is suitable only for products that can tolerate accumulation.

It operates using gates on the infeed lanes, which release the product rows in sequence, and requires two conditions: the products must be able to withstand pressure during accumulation, and the downstream machine must be capable of receiving products in a continuous train without being adversely affected.

The second requirement has a specific technical reason. At the outlet, the products are close together or touching. When this train reaches the downstream machine, the instantaneous speed seen by the machine is therefore twice the average speed. Either the downstream equipment must be able to handle this, or the flow must be normalised using a deceleration conveyor followed by an acceleration conveyor, at the cost of a larger footprint, two additional motors and more complex control logic.

The pneumatic solution is also well suited to a particular application: where the carton itself is the primary package, as is common in the pasta industry, in the section between secondary packaging and the case packer, where the product can be accumulated.

When, on the other hand, the product is delicate or must be handled without contact, dynamic lane mergers are used. M.H. offers two series.

The DU Series merges products by reducing the number of lanes through anti-overlap timing belts operating at controlled differential speeds, one for each infeed lane. Products are handled individually and without contact, making the system suitable for fragile products or products prone to overlapping, at speeds of up to approximately 240 pieces per minute.

The HP Series is the evolution of the DU Series, developed specifically for high-speed flow-wrapping lines and for connections between primary and secondary packaging. In this case, pressure is completely eliminated because the products must never come into contact. Each item is individually timed by means of a multi-belt system with independent brushless drives for every infeed lane, combined with blower-generated vacuum for higher acceleration rates, reaching up to 600 pieces per minute at the outlet. In flow-wrapping applications, precise product timing is essentially mandatory, as it is the only way to prevent products from overlapping.

Outlet pitch: a detail that should not be underestimated

As speed increases, it becomes essential to achieve the most consistent possible product pitch at the outlet of the lane merger, because this determines how the downstream machine receives each item.

A product flow delivered in trains can push the downstream machine beyond its production limits because of the instantaneous speed peaks described above. Individual product timing, on the other hand, controls the distance between packs and transfers them without contact, reducing the risk of jams and overlaps.

The choice always starts with the product

In every case, the starting point is always the product. The first step is to determine whether it can withstand accumulation, then assess its fragility and shape, the required production rate and the number of lanes to be merged, and finally the type of downstream machine, particularly whether it is a flow wrapper positioned between primary and secondary packaging.

The right technology emerges from these answers: a pneumatic lane merger for products that can withstand pressure, the DU Series for products requiring contact-free handling, and the HP Series for high-speed flow-wrapping applications.

At M.H. Material Handling, we manufacture material-handling systems and efficiency solutions for packaging lines in the food industry and related sectors. Over more than forty years of field experience, from food & beverage to pharmaceuticals and packaging, we have developed the expertise required to identify where lane merging can make a real difference and where it is unnecessary. On this basis, we design customised pneumatic and dynamic lane mergers from the DU and HP Series, starting with an analysis of the production line.

If you are planning a new line or a revamping project and lane merging is still an open issue, we can assess it together to identify the most suitable configuration.

Is your packaging line inefficient? Just add a buffer and the problem is solved.

Or at least, that’s what many people think.

Adding a buffer to an existing line can turn into an expensive and unnecessary investment. Before proceeding with the installation, carefully assess all the preliminary factors: an in-depth analysis can help you avoid ending up with the same problems you started with.

To identify the most suitable solution for your packaging line, contact us: we’ll analyse your specific case and help you define the most effective solution.